Blog by Sanwariya Packaging

Your Trusted Partner in Packaging

Learn About Our Vision for the Future And Grow with Us.

Your Trusted Partner in Pharma Packaging

Learn about our vision for the future and grow with us.

Your Trusted Partner
in Pharma Packaging

Learn about our vision for the future and grow with us.

Know More

Tag: pharmaceutical foil

Importance of strong foil in pharmacy dispensing

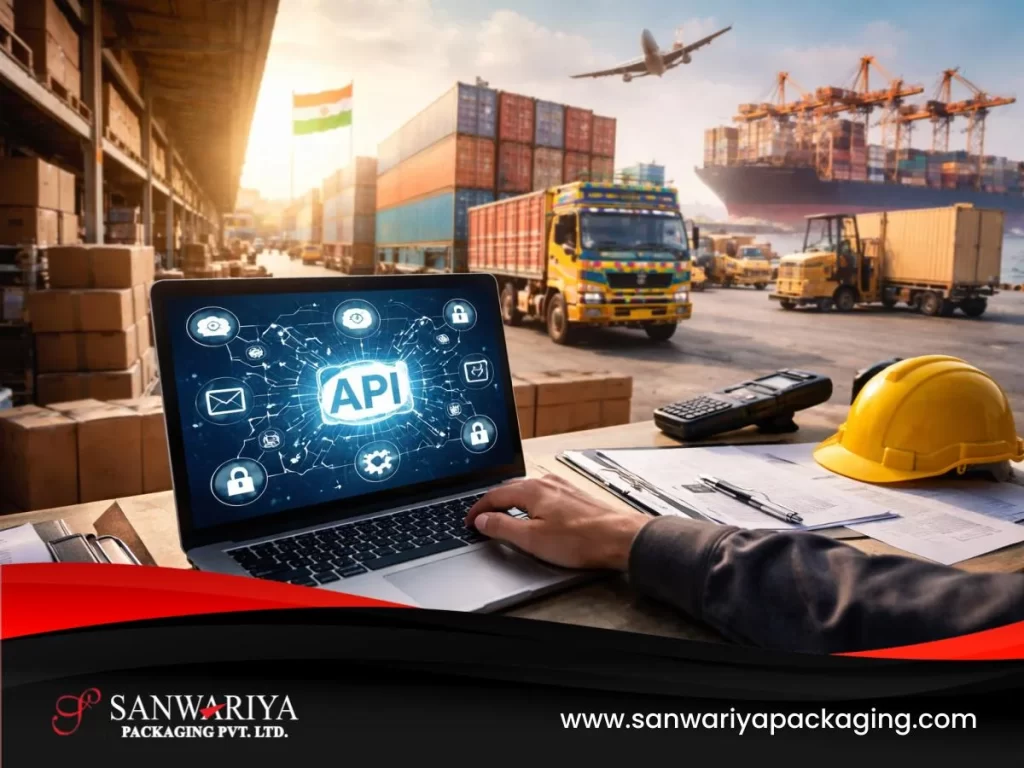
Modern pharmaceutical supply chains often extend across continents. Medicines manufactured in one country may travel thousands of kilometers before reaching distributors, pharmacies, and ultimately patients. During this journey, pharmaceutical products may face fluctuating temperatures, high humidity levels, mechanical stress, and prolonged storage conditions.

For formulations containing sensitive Active Pharmaceutical Ingredients (APIs), these environmental factors can pose significant stability risks. As a result, packaging plays a critical role in maintaining product quality throughout global logistics networks. Selecting the correct blister foil structure helps ensure that medicines remain safe, effective, and stable even after long transit periods.

Why Long Supply Chains Create Stability Challenges

Unlike many consumer products, pharmaceutical medicines must maintain strict quality and stability parameters from manufacturing to patient use. Long-distance transportation introduces multiple stages where environmental conditions may vary.

Shipments frequently move through trucks, shipping containers, cargo aircraft, and distribution warehouses. At each stage, exposure to temperature variation, humidity, and mechanical vibration can occur. Over time, these environmental stresses may affect both the packaging and the product inside.

For APIs that are sensitive to moisture, oxygen, or light, inadequate packaging protection can increase the risk of degradation during transit. Therefore,  pharmaceutical packaging must be designed not only for storage stability but also for real-world supply chain conditions.

Supply Chain Journey Conditions

International pharmaceutical distribution often involves complex logistics routes. A single shipment may move through several countries, climate zones, and transportation modes before reaching the final destination.

Sea freight, which is commonly used for global pharmaceutical distribution, can take several weeks depending on the route. During this period, containers may experience high humidity levels, especially when traveling through tropical or coastal regions.

In addition to environmental exposure, products may also remain in temporary storage at ports, warehouses, and customs facilities. These extended holding periods increase the importance of packaging materials that can maintain strong barrier performance over time.

Understanding the complete supply chain journey helps packaging teams select materials capable of protecting pharmaceutical products during prolonged logistics timelines.

The Role of Humidity Protection

Humidity is one of the most significant environmental threats to pharmaceutical stability during long-distance transportation. Many APIs are sensitive to moisture and can undergo hydrolysis reactions when exposed to elevated humidity levels.

Even small amounts of water vapor entering blister cavities can gradually affect product stability over extended transit periods. High humidity environments combined with long shipping durations can accelerate degradation processes if packaging barriers are insufficient.

High-barrier aluminum blister foils significantly reduce moisture vapor transmission, helping protect the internal environment of each blister cavity. By maintaining a stable microenvironment around the medicine, these barrier materials play a crucial role in preserving API integrity during international shipping.

Mechanical Stress During Transportation

Pharmaceutical products encounter repeated handling throughout the supply chain. Cartons are stacked on pallets, transported by trucks, transferred between warehouses, and loaded onto ships or aircraft.

These operations introduce vibrations, compression forces, and occasional impacts that can stress packaging structures. If blister packs lack adequate mechanical strength, cavities may deform or seals may weaken, potentially allowing environmental intrusion.

Durable pharmaceutical foil structures help maintain seal integrity and cavity stability even under challenging logistics conditions. Strong blister materials reduce the likelihood of packaging damage and help ensure that each dose remains properly protected until it reaches the patient.

Selecting the Correct Barrier Structure

Packaging engineers must evaluate several factors when selecting blister foil structures for products intended for long-distance export. The sensitivity of the API, expected transit duration, and environmental conditions along the shipping route all influence packaging requirements.

Standard blister foil structures may be suitable for domestic distribution or short supply chains. However, products shipped across international routes often require enhanced barrier performance.

Aluminum-based blister foils provide excellent protection against moisture, oxygen, and light. These materials are commonly used for formulations that require high levels of environmental protection during storage and transportation.

By aligning packaging design with logistics realities, pharmaceutical companies can significantly reduce the risk of stability issues during transit.

Packaging Considerations for Export Markets

Global pharmaceutical distribution requires careful coordination between formulation scientists, packaging development teams, and supply chain specialists. Export markets may present environmental conditions that differ significantly from domestic storage environments.

Certain regions experience consistently high humidity, while others may have extreme seasonal temperatures. These environmental variations must be considered when qualifying packaging systems for international distribution.

High-barrier blister packaging helps maintain product stability despite these environmental differences. Reliable packaging solutions support consistent medicine quality regardless of how far the product must travel before reaching healthcare providers and patients.

Maintaining API Stability Across Global Supply Chains

Long-distance pharmaceutical distribution exposes medicines to humidity, temperature changes, mechanical vibration, and extended storage timelines. Effective blister packaging plays a critical role in protecting sensitive APIs from these environmental risks during international transportation.

By selecting high-barrier pharmaceutical foil structures with strong moisture protection and mechanical durability, pharmaceutical manufacturers can maintain product stability throughout complex logistics networks. Proper packaging selection helps ensure medicines retain their safety, potency, and quality from manufacturing facilities to patients worldwide.

Sanwariya Packaging manufactures pharmaceutical aluminum foils designed to provide strong moisture barriers, consistent sealing performance, and reliable mechanical stability for blister packaging applications. Through advanced manufacturing processes and strict quality controls, Sanwariya Packaging supports pharmaceutical companies in protecting API stability across long global supply chains and challenging transit environments.

Packaging strategies to protect APIs across supply chains

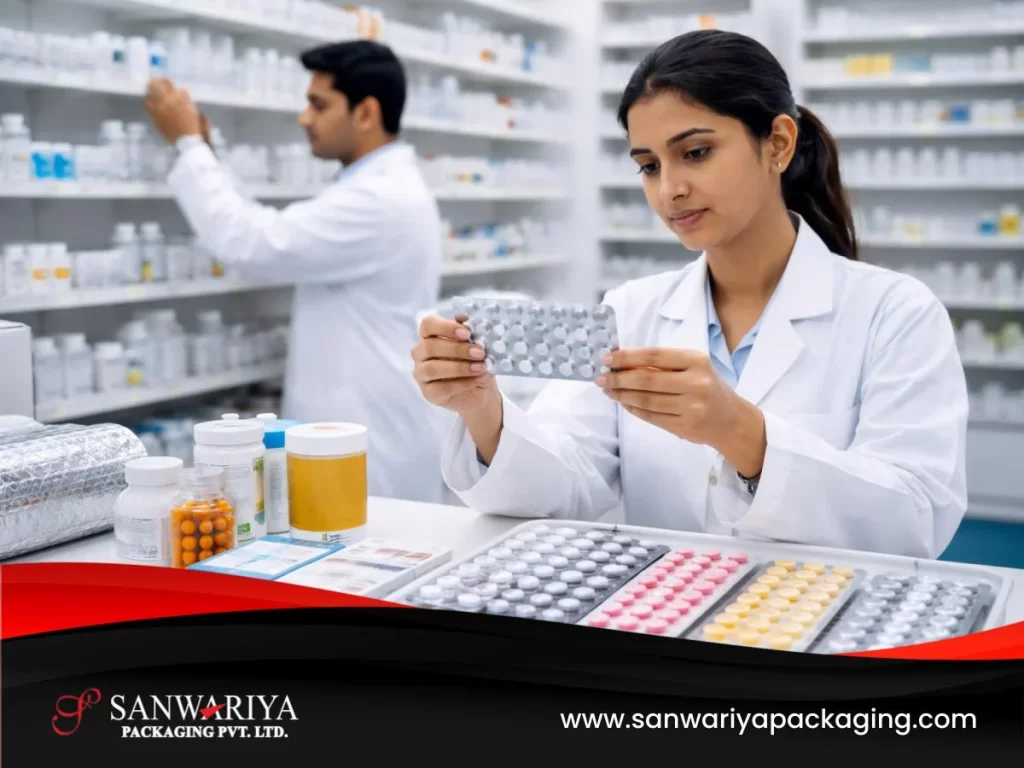
Pharmaceutical packaging must protect medicines not only during manufacturing and transportation but also during the final stages of the supply chain. One of the most demanding environments for packaging materials is the pharmacy dispensing stage. 

In hospitals, retail pharmacies, and clinical settings, blister packs are frequently handled by pharmacists, technicians, and patients. During this stage, packaging materials are exposed to repeated handling, pressure, and mechanical stress. 

If blister foils are not sufficiently durable, they may tear prematurely, puncture easily, or compromise the protection of the medicine inside. Because of this, the mechanical strength and durability of pharmaceutical foil are critical considerations during packaging development. 

This blog explains why durable blister foils are important in pharmacy environments, how tear strength and puncture resistance contribute to packaging performance, and how pharmaceutical companies ensure that packaging materials remain reliable throughout dispensing and patient use.

Packaging Stress in Pharmacy Dispensing Environments

Pharmacy dispensing environments involve frequent manual handling of medicine packs. Pharmacists and technicians often remove individual doses from larger packaging units, verify labeling information, and prepare medicines for patient distribution.

During these routine activities, blister packs may experience several types of mechanical stress.

  • Repeated bending or flexing of blister cards
  • Pressure applied while separating doses
  • Contact with dispensing equipment or storage trays
  • Handling during patient counseling and medication preparation

These handling conditions can place significant strain on blister foil structures. If the foil material is too fragile, it may tear unintentionally or fail to maintain the integrity of the blister cavity.

Durable foil materials help ensure that the packaging continues to protect the medicine until the moment of use.

Importance of Tear Strength in Blister Foils

Tear strength refers to the ability of a material to resist tearing when a force is applied. In pharmaceutical blister packaging, appropriate tear strength is necessary to maintain packaging integrity while still allowing the medicine to be dispensed intentionally.

If foil tear strength is too low, several problems may occur:

  • Accidental Tearing During Routine Handling
  • Exposure Of The Medicine Before Intended Use
  • Reduced Protection From Environmental Factors
  • Potential Contamination Risks

On the other hand, foil should not be excessively difficult to open. Packaging must balance durability with accessibility to ensure that patients can remove medicines without excessive effort.

Packaging engineers therefore design foil structures that provide controlled tearing during the push-through dispensing process.

Puncture Resistance and Blister Protection

Puncture resistance is another important property of durable blister foil. This refers to the ability of the material to resist penetration by external pressure or sharp contact.

During pharmacy handling and transportation, blister packs may be exposed to objects that apply localized pressure.

Examples may include:

  • Contact With Sharp Edges Of Storage Trays
  • Compression Within Medication Carts
  • Stacking Of Packaged Medicines
  • Accidental Impacts During Handling

If the foil surface punctures easily, the protective barrier around the medicine may be compromised.

Foils with strong puncture resistance help maintain the protective seal around each blister cavity and reduce the risk of accidental exposure.

Balancing Durability and Patient Accessibility

Pharmaceutical packaging must remain strong enough to protect the product while still allowing patients to access the medicine easily.

Designing blister foils requires careful consideration of patient usability factors.

Key design considerations include:

  • Controlled Push-Through Performance
  • Resistance To Accidental Tearing During Handling
  • Accessibility For Elderly Or Limited-Strength Patients
  • Consistent Opening Performance Across Blister Cavities

Packaging development teams often conduct usability evaluations to ensure that the blister pack remains easy to open without compromising durability.

Achieving this balance helps support safe and convenient medication use.

Mechanical Stability During High-Volume Pharmacy Use

In hospital pharmacies and large dispensing centers, medicines may be handled in high volumes every day. Blister packs are frequently stored in automated dispensing cabinets, medication carts, or inventory trays.

These environments place repeated mechanical stress on packaging materials.

Potential stress factors include:

  • Frequent Insertion And Removal From Storage Systems
  • Vibration During Movement Of Dispensing Carts
  • Pressure From Stacked Packaging Units
  • Repeated Manual Handling By Pharmacy Staff

Foil structures with strong mechanical stability help maintain packaging performance even under these demanding conditions.

Reliable packaging durability supports smooth pharmacy operations and reduces the risk of damaged medicine packs.

Quality Testing for Foil Durability

Before  pharmaceutical packaging materials are approved for production use, they typically undergo testing to evaluate mechanical strength and durability.

These tests help confirm that the foil structure can withstand expected handling conditions throughout the supply chain.

Common durability evaluations may include:

  • Tear Resistance Testing
  • Puncture Resistance Measurements
  • Push-Through Force Testing For Blister Packs
  • Simulated Handling And Transport Tests

Quality assurance teams review the results of these tests to ensure that packaging materials meet both functional and regulatory expectations.

Maintaining documented testing procedures also supports compliance with pharmaceutical quality systems.

Ensuring Safe Dispensing and Patient Protection

Durable blister foil plays an important role in maintaining the integrity of  pharmaceutical packaging from production to patient use. In pharmacy environments where medicines are frequently handled, strong foil materials help prevent accidental damage and preserve the protective barrier around each dose.

By combining appropriate tear strength, puncture resistance, and controlled opening performance, pharmaceutical packaging can remain reliable throughout dispensing and patient use.

Durable foil structures contribute to safe medication handling, clear product identification, and consistent packaging performance across healthcare environments.

Sanwariya Packaging manufactures pharmaceutical aluminum foils designed to provide reliable mechanical strength, consistent sealing performance, and stable printing quality for blister packaging applications. Through advanced manufacturing processes and strict quality controls, Sanwariya Packaging supports pharmaceutical companies in developing durable packaging solutions suitable for demanding pharmacy dispensing environments.

Proper handling, storage, and transport of pharma foil

Pharmaceutical products distributed internationally must comply with labeling regulations across multiple countries. In many markets, medicines are required to display information in more than one language to ensure that patients and healthcare professionals clearly understand product details and usage instructions. 

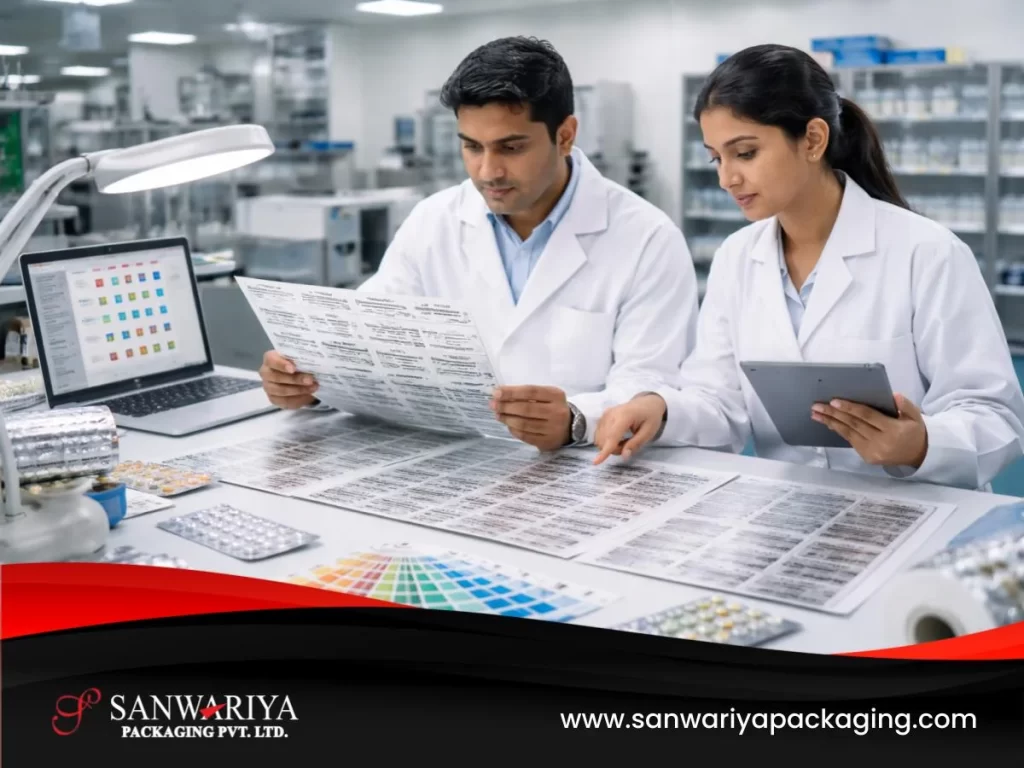
As a result, pharmaceutical packaging often needs to accommodate multilingual text while maintaining readability, regulatory compliance, and accurate information presentation. Printed aluminum blister foils frequently carry important product information such as medicine names, dosage strengths, batch details, manufacturing information, and storage instructions. 

When these details must appear in multiple languages, careful layout design becomes essential. Font size, text spacing, line order, and translation accuracy must all be managed to ensure that information remains clear and compliant. 

This blog explains how pharmaceutical companies design foil text layouts for multilingual export markets and highlights the importance of font selection, regulatory text structure, and error-free translations in multilingual pharma foil printing.

Why Multilingual Packaging Is Required in Global Markets

Pharmaceutical companies exporting medicines to international markets must follow the labeling requirements established by local regulatory authorities. Many regions require medicines to display product information in multiple languages to support safe usage and patient understanding.

Multilingual packaging helps ensure that essential product information is accessible to a diverse population.

Common reasons for multilingual labeling include:

  • Regulatory requirements in multilingual regions
  • Patient safety and accessibility considerations
  • Clear communication for healthcare professionals
  • Standardized labeling across export markets

Countries or regions with multiple official languages often require bilingual or multilingual labeling to ensure that product information is understood by all users.

When blister foils contain printed product information, the layout must accommodate these language requirements without compromising readability.

Challenges of Multilingual Text on Blister Foils

Blister foils have limited printable space, especially when compared with outer cartons or patient information leaflets. This limited surface area makes multilingual layout design more complex.

Adding multiple languages to the same foil requires careful planning to ensure that each line of text remains readable and correctly aligned.

Common challenges include:

  • Limited space for multiple language blocks
  • Variations in word length between languages
  • Maintaining clear spacing between text lines
  • Preserving readability on small blister cavities
Packaging development teams must design layouts that balance space constraints with regulatory labeling requirements. Proper planning during the artwork stage helps prevent overcrowded or difficult-to-read packaging.

Font Size and Spacing Considerations

Maintaining readable text is one of the most important aspects of multilingual pharmaceutical labeling. Font sizes must be large enough to remain legible while still fitting within the available print area on the foil.

Several design considerations help maintain readability:

  • Consistent font sizes across languages
  • Adequate spacing between lines of text
  • Clear separation between language sections
  • Avoidance of overly condensed fonts
Spacing becomes particularly important when multiple languages appear on a single foil surface. If text is too closely spaced, it may become difficult to read after printing or during product handling. Packaging artwork teams therefore evaluate layout designs carefully before finalizing the print artwork.

Regulatory Line Order and Information Hierarchy

Regulatory guidelines often specify the order in which certain information must appear on pharmaceutical packaging. This includes elements such as the product name, dosage strength, manufacturing details, batch number, and expiration date.

When designing multilingual layouts, the structure of this information must remain consistent across all languages.

Typical layout considerations may include:

  • Placing critical product identification details in a prominent position
  • Maintaining the same information sequence across languages
  • Ensuring regulatory text remains clearly visible
  • Avoiding overlap between different language blocks

Maintaining a logical information hierarchy helps ensure that healthcare professionals and patients can quickly identify important product details.

Packaging designs must therefore balance regulatory structure with available print space.

Preventing Translation Errors in Packaging Artwork

Accurate translation is essential when pharmaceutical packaging is printed in multiple languages. Even small translation errors can create confusion or lead to regulatory compliance issues.

To prevent such risks, pharmaceutical companies often follow structured translation verification processes.

These processes may include:

  • Professional medical translation services
  • Review by regulatory or medical specialists
  • Cross-checking translations against approved product documentation
  • Final proofreading before artwork approval

Because blister foils are printed in large production volumes, translation accuracy must be confirmed before printing begins.

Correcting errors after production can result in material waste or packaging delays.

Printing Precision and Layout Stability

Printing multilingual text on aluminum foil requires precise alignment and consistent print quality. Small variations in print registration or layout alignment may affect text readability, especially when multiple language blocks appear close together.

Production teams monitor several factors to maintain layout accuracy:

  • Precise printing registration across foil reels
  • Stable ink density for small text characters
  • Controlled printing pressure to maintain clarity
  • Consistent alignment of repeated blister patterns

Maintaining stable printing conditions ensures that multilingual text remains clear and readable across the entire production batch.

Reliable printing processes are therefore essential for high-quality multilingual pharma foil printing.

Export Market Considerations for Multilingual Packaging

Pharmaceutical companies supplying medicines to multiple regions often manage several packaging variations to meet local language requirements.

Export teams work closely with packaging and regulatory departments to ensure that each market receives compliant packaging.

Important considerations for export packaging may include:

  • Adapting packaging artwork for region-specific language requirements
  • Ensuring translations meet local regulatory guidelines
  • Managing multiple artwork versions for different markets
  • Maintaining consistency across packaging materials

These processes help ensure that medicines distributed internationally meet both regulatory expectations and patient communication needs.

Supporting Clear Communication Across Global Markets

Multilingual pharmaceutical packaging plays an important role in ensuring that medicine information is accessible to patients and healthcare professionals around the world. Designing foil text layouts for multiple languages requires careful attention to font sizing, spacing, information hierarchy, and translation accuracy.

By following structured artwork design practices and maintaining precise printing control, pharmaceutical companies can produce packaging that remains clear, compliant, and easy to read across international markets.

Effective multilingual labeling helps reduce communication barriers and supports safe medicine use in diverse healthcare environments.

Sanwariya Packaging manufactures printed pharmaceutical aluminum foils designed to support precise text reproduction, consistent print alignment, and high-quality multilingual printing. Through advanced printing capabilities and controlled production processes, Sanwariya Packaging helps pharmaceutical companies deliver packaging solutions that maintain clarity and regulatory compliance across global export markets.

Designing foil text for multi-language markets

Pharmaceutical aluminum foil is a critical packaging material used in blister packaging to protect medicines from moisture, oxygen, light, and external contamination. While foil structures are designed to provide strong barrier performance, their protective properties must be preserved throughout the supply chain. 

Improper handling, storage, or transportation can damage the foil surface, affect sealing performance, or compromise print quality. Because of this, pharmaceutical companies follow strict procedures when storing and transporting foil reels. 

Controlled environmental conditions, careful reel handling, and systematic inspection help ensure that packaging materials remain in optimal condition before entering the packaging line. 

This blog explains recommended pharma foil storage guidelines, including temperature and humidity control, proper reel handling practices, transportation considerations, and inspection procedures for incoming materials.

Why Proper Handling of Pharma Foil Matters

Pharmaceutical foil is manufactured under controlled conditions to meet strict quality and barrier performance requirements. However, the material can still be affected by environmental exposure or physical damage during storage and transportation.

Improper foil handling may lead to several issues:

  • Dents or deformation of foil reels
  • Damage to printed surfaces
  • Contamination of the foil surface
  • Reduced sealing performance during blister packaging

Even minor physical damage can affect packaging line performance. For example, uneven reels may cause feeding problems during high-speed blister packaging operations.

Maintaining proper handling procedures helps preserve the structural integrity and print quality of the foil.

Temperature and Humidity Control for Foil

Environmental conditions play an important role in maintaining the quality of pharmaceutical packaging materials. Excessive humidity or temperature fluctuations may affect coatings, adhesives, or printing layers applied to the foil.

Warehouses storing pharmaceutical foils typically maintain controlled environmental conditions.

Important environmental controls for foil include:

  • Stable temperature conditions within recommended storage ranges
  • Relative humidity control to prevent moisture exposure
  • Avoidance of direct sunlight or heat sources
  • Protection from sudden environmental fluctuations

Maintaining stable environmental conditions helps prevent condensation or surface degradation that could affect packaging performance.

Controlled storage environments also support compliance with pharmaceutical quality management systems.

Best Practices for Reel Handling

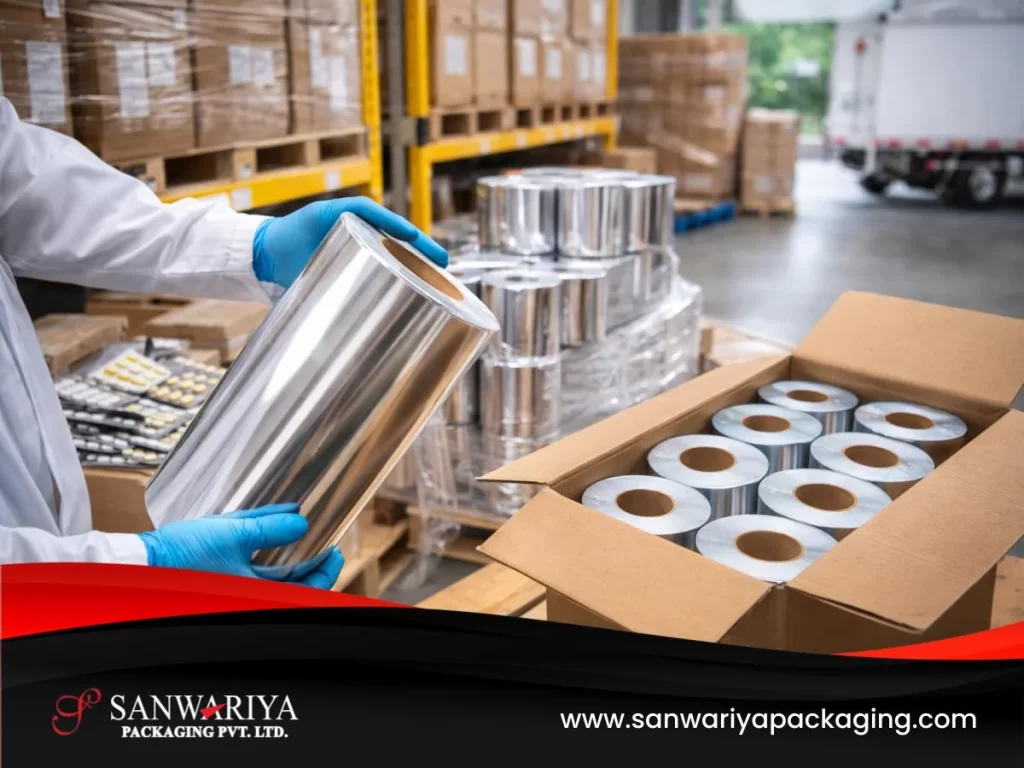
Pharmaceutical foil is usually supplied in large reels that must be handled carefully during transportation, storage, and transfer to packaging lines.

Improper handling may cause physical damage such as edge dents, crushed cores, or surface scratches.

Recommended reel handling practices include:

  • Using appropriate lifting equipment designed for reel handling
  • Avoiding rolling reels directly on warehouse floors
  • Protecting reel edges from impact damage
  • Keeping reels in their original protective packaging until use
Handling procedures should also ensure that the reels remain properly aligned to prevent deformation. Careful reel handling helps maintain smooth operation during blister packaging production.

Preventing Mechanical Damage During Storage

Mechanical damage is one of the most common causes of foil rejection during incoming material inspections.

Damage may occur when reels are stacked improperly or when heavy objects are placed on top of packaging materials.

Warehouses storing pharmaceutical foil typically follow several protective practices.

  • Storing reels vertically on stable pallets
  • Maintaining sufficient spacing between stacked materials
  • Preventing contact with sharp edges or heavy equipment
  • Ensuring stable stacking to avoid reel movement

Proper storage arrangements help protect both the foil surface and the structural integrity of the reel.

Maintaining clean and organized warehouse environments also reduces the risk of contamination.

Transportation and Logistics Considerations

Pharmaceutical foil often travels long distances before reaching the packaging facility. During transportation, packaging materials may be exposed to vibrations, environmental changes, or handling by multiple logistics providers.

To reduce these risks, foil reels are usually transported using protective packaging and secure palletization.

Key transportation considerations include:

  • Stable pallet stacking to prevent movement during transit
  • Protective wrapping to shield reels from dust and moisture
  • Shock protection to reduce vibration-related damage
  • Climate-aware transportation for sensitive materials

Export shipments may also require additional precautions, particularly when transporting materials through regions with extreme environmental conditions.

Proper logistics planning helps ensure that packaging materials arrive in usable condition.

Inspection of Foil Reels on Receipt

Quality control procedures typically require inspection of incoming packaging materials before they are released for production use.

Incoming inspection helps confirm that the materials received meet approved specifications and have not been damaged during transportation.

Common inspection checks may include:

  • Verification of reel identification and batch documentation
  • Visual inspection for dents, scratches, or surface damage
  • Confirmation of protective packaging integrity
  • Review of storage conditions during transport if required
If any issues are identified during inspection, the material may be placed on hold for further evaluation. These inspection steps help maintain quality control within pharmaceutical packaging operations.

Warehouse Inventory and Stock Rotation

Proper inventory management helps ensure that packaging materials are used within their recommended storage period.

Pharmaceutical warehouses often follow structured inventory systems that track material batches and storage durations.

Common inventory management practices include:

  • First-in, first-out (FIFO) material usage
  • Clear batch identification and labeling
  • Regular warehouse condition monitoring
  • Documentation of storage conditions and handling procedures

Following these practices ensures traceability and helps maintain packaging material performance throughout storage.

Inventory control is an important part of pharmaceutical quality management systems.

Maintaining Packaging Material Integrity Across the Supply Chain

Pharmaceutical packaging materials must maintain consistent quality from manufacturing to final use on packaging lines. Proper handling, storage, and transportation procedures help ensure that foil reels remain free from damage and environmental exposure.

Following established pharma foil storage guidelines supports reliable blister packaging performance, protects printing quality, and helps maintain regulatory compliance within pharmaceutical manufacturing environments.

Supply chain teams, warehouse managers, and quality control personnel all play an important role in protecting packaging materials throughout their lifecycle.

Sanwariya Packaging manufactures pharmaceutical aluminum foils designed for reliable barrier performance, stable printing, and compatibility with high-speed blister packaging systems. Through controlled manufacturing processes and secure packaging practices supported by its infrastructure, Sanwariya Packaging supports pharmaceutical companies in maintaining the integrity of packaging materials throughout global storage and distribution.

For further information or requirements, you can get in touch with us or directly request a quote.

Serialization updates for printed foils in 2026

Medicines are carefully formulated to remain stable and effective throughout their shelf life. However, some pharmaceutical compounds are highly sensitive to light, particularly ultraviolet (UV) radiation. When exposed to light, these medicines may undergo chemical degradation that reduces potency or alters their safety profile.

Because of this risk, protecting medicines from light exposure is an important consideration during pharmaceutical packaging design. Packaging materials must shield sensitive formulations from harmful wavelengths while maintaining stability during storage, transportation, and distribution.

Blister packaging using aluminum-based foils plays a significant role in protecting light-sensitive medicines. The reflective properties of aluminum, combined with specialized coatings, help prevent ultraviolet radiation from reaching the drug product.

This blog explains the science of UV degradation, how aluminum foil provides light protection, the testing methods used to validate UV resistance, and how pharmaceutical companies select the most appropriate foil structures for light-sensitive medicines.

Why Light Exposure Can Damage Medicines

Many pharmaceutical ingredients are sensitive to electromagnetic radiation within the ultraviolet and visible light spectrum. When exposed to light, the energy absorbed by the molecule can trigger chemical reactions that alter the structure of the active ingredient.

These reactions may lead to several types of degradation.

  • Loss of drug potency
  • Formation of degradation by-products
  • Color changes in the formulation
  • Reduced shelf life or stability

Certain categories of medicines are particularly vulnerable to photodegradation. These may include antibiotics, vitamins, biological compounds, and formulations containing complex organic molecules.

Even limited exposure during transportation or storage can contribute to gradual degradation if packaging does not provide adequate protection.

For this reason, stability studies often include light exposure testing to determine whether protective packaging is required.

Understanding UV Degradation in Pharmaceutical Stability

Photodegradation occurs when molecules absorb photons from light energy. Ultraviolet radiation carries higher energy compared with visible light, making it especially capable of breaking chemical bonds.

In pharmaceutical stability studies, exposure to light can cause molecular reactions such as oxidation, isomerization, or structural breakdown of active ingredients.

The likelihood of degradation depends on several factors.

  • Wavelength of the incoming light
  • Duration of exposure
  • Sensitivity of the drug molecule
  • Transparency of the packaging material

Packaging materials that allow UV light to pass through may expose the product to degradation risks over time. As a result, selecting materials with strong UV-blocking properties is an important part of packaging development for light-sensitive medicines.

How Aluminum Foil Acts as a UV Barrier

Aluminum foil provides one of the most effective barriers against light exposure in pharmaceutical packaging. Unlike transparent or translucent materials, aluminum reflects and blocks a large portion of incoming radiation.

The metal surface reflects both visible and ultraviolet wavelengths, preventing light from reaching the medicine inside the blister cavity.

This reflective behavior provides several advantages.

  • Near-complete opacity to light
  • Strong UV blocking capability
  • Stable protection across different wavelengths
  • Consistent performance during storage and transport

Because of these properties, aluminum foil is widely used in blister foils for light-sensitive formulations.

When combined with appropriate coatings and printing layers, foil structures can maintain both functional protection and regulatory labeling requirements.

Reflectivity Advantage of Aluminum in Pharmaceutical Packaging

The reflective surface of aluminum plays a key role in reducing UV penetration. When ultraviolet radiation strikes the foil surface, a significant portion of the energy is reflected away instead of passing through the material.

This reflective behavior helps maintain a stable internal environment for the medicine.

The performance of the foil barrier can be influenced by factors such as:

  • Foil thickness
  • Coating layers applied to the surface
  • Printing inks and pigments
  • Surface finish of the foil

Higher-quality foil structures maintain consistent reflectivity while also supporting reliable printing and sealing performance.

This combination of mechanical strength and optical protection makes aluminum foil particularly suitable for medicines that require strict light protection, including advanced structures like cold forming foils and multi-layer foils.

Testing Light Protection in Pharmaceutical Packaging

Pharmaceutical companies must demonstrate that packaging materials adequately protect light-sensitive medicines throughout the product’s shelf life.

This evaluation is typically performed during stability testing under controlled laboratory conditions.

Common testing approaches include:

  • Exposure to defined ultraviolet and visible light levels
  • Accelerated stability testing with controlled light sources
  • Measurement of degradation products after exposure
  • Comparison of protected and unprotected samples

International stability guidelines often define the total light exposure conditions required for photostability testing.

These tests help determine whether the selected packaging structure provides sufficient UV protection for the medicine.

If degradation is observed, packaging engineers may modify the material structure or increase the protective barrier properties.

Selecting the Right Foil Coating for UV Protection

While aluminum itself provides strong light protection, coatings and printing layers applied to the foil can influence overall performance.

Coatings are often applied to support sealing, printing, or machine compatibility. However, these coatings must also maintain the protective characteristics of the foil.

Packaging development teams evaluate several coating-related factors.

  • Compatibility with blister sealing processes
  • Resistance to environmental exposure
  • Stability of printed graphics during storage
  • Maintenance of UV-blocking performance

Specialized coatings may also reduce surface reflections that could interfere with printing or scanning technologies while maintaining the underlying barrier performance.

Selecting the correct coating system ensures that the foil continues to provide effective UV protection throughout the product lifecycle.

Challenges When Shipping Light-Sensitive Medicines Globally

Medicines distributed internationally may encounter a wide range of environmental conditions during transportation. Products shipped to regions with strong sunlight or high ambient temperatures may experience greater light exposure during handling and storage.

Export-oriented pharmaceutical companies therefore evaluate packaging carefully when shipping to high-exposure markets.

Potential risks during distribution include:

  • Prolonged exposure to sunlight during logistics handling
  • Storage in brightly lit warehouse environments
  • Transportation through regions with intense solar radiation

Using packaging materials with strong light barrier properties helps reduce these risks and ensures that medicines remain stable until they reach patients.

Regulatory Expectations for Photostability Protection

Global pharmaceutical regulators expect companies to demonstrate that packaging materials adequately protect medicines from environmental factors such as light, moisture, and oxygen.

Photostability studies form part of the broader stability testing framework used to establish shelf life.

Regulatory documentation may include:

  • Photostability study reports
  • Packaging material specifications
  • Validation of protective packaging performance
  • Long-term stability data under recommended storage conditions

Maintaining thorough documentation helps ensure compliance during regulatory submissions and inspections.

Packaging materials must therefore be selected not only for functional performance but also for their ability to support documented stability outcomes.

Ensuring Stability for Light-Sensitive Medicines

Protecting medicines from ultraviolet radiation is an essential aspect of pharmaceutical packaging design. Exposure to light can cause chemical degradation that affects both product efficacy and safety.

Aluminum blister foils provide an effective solution by reflecting and blocking ultraviolet radiation before it reaches the medicine. When combined with appropriate coatings and carefully designed packaging structures, these materials help maintain stability throughout the product’s lifecycle.

For pharmaceutical companies developing light-sensitive formulations, selecting the right packaging materials is a critical step in ensuring long-term product quality and regulatory compliance.

Sanwariya Packaging manufactures pharmaceutical aluminum foils designed to provide strong barrier protection, reliable printing performance, and compatibility with modern blister packaging systems. Through controlled manufacturing processes and advanced capabilities supported by its infrastructure, Sanwariya Packaging supports pharmaceutical companies in developing packaging solutions that help protect sensitive medicines throughout global distribution.For further discussions or requirements, you can get in touch with us or directly request a quote.

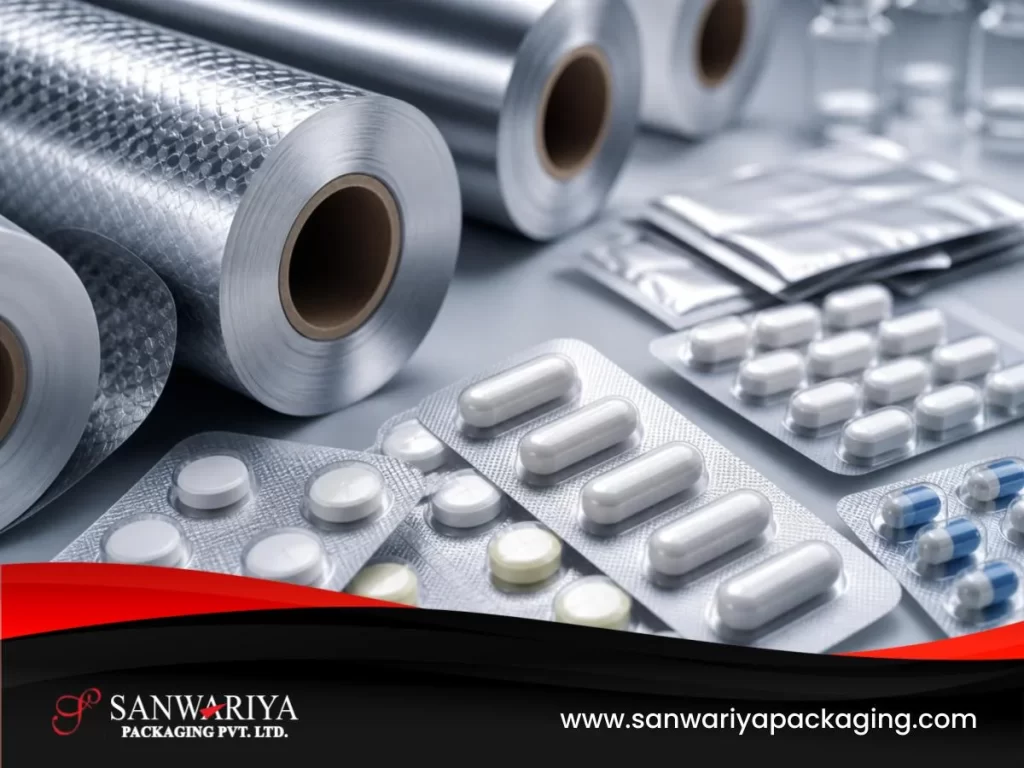
Pharmaceutical blister packs and aluminum foil rolls used for seal integrity in packaging

Pharmaceutical packaging must ensure that medicines remain stable, effective, and safe throughout their lifecycle. Among the most widely used formats, blister and strip packaging rely heavily on one critical factor: seal integrity.

While sealing performance is influenced by multiple variables, one of the most decisive factors is the quality and consistency of the aluminum foil used.

If seals are compromised due to material inconsistencies or poor coating performance, moisture, oxygen, or contaminants can enter the pack—leading to product degradation well before expiry. For pharmaceutical manufacturers, this directly impacts product quality, compliance, and market reputation.

This article focuses on how foil properties and sealing compatibility drive seal integrity in blister and strip packaging.

Why Seal Integrity Is a Material-Driven Parameter

Both blister and strip packaging depend on sealed structures for protection.

Blister Packaging

  • Forming film (PVC or similar)
  • Aluminum lidding foil with heat-seal coating

Strip Packaging

  • Laminated aluminum foils (with polymer layers such as LDPE)

In both cases, the seal is only as reliable as the material interface between layers.

Even when sealing parameters are optimized, poor foil quality can lead to:

  • inconsistent bonding
  • micro-leakage paths
  • reduced barrier performance
  • variability across production batches
For sensitive pharmaceutical formulations, such inconsistencies can result in stability failures and compliance risks.

Seal Strength in Blister Packaging

Blister packaging uses non-peelable seals, where the lidding foil is bonded permanently to the forming film.

The performance of this seal depends largely on the heat-seal coating applied to the aluminum foil.

Critical material-driven factors include:

  • uniform coating thickness across the foil surface
  • consistent adhesion properties with the forming film
  • resistance to channel formation or weak spots
  • compatibility with different blister substrates (PVC, PVDC, etc.)

Unlike strip packaging, the seal is not designed to be peeled. Instead, it must maintain integrity until the product is accessed via push-through.

Peel Strength in Strip (Laminated) Packaging

Peel strength is a relevant parameter in strip packaging, where laminated foil structures are used.

In these systems, aluminum foil is combined with polymer layers (such as LDPE), enabling controlled peel-open functionality.

Peel strength depends on:

  • the lamination quality between layers
  • the polymer composition and thickness
  • the consistency of bonding across the laminate

A well-designed laminate ensures:

  • secure sealing during storage and transport
  • predictable and user-friendly opening
This parameter is specific to laminated strip foils and does not apply to standard blister lidding foils.

Key Foil Properties That Influence Seal Integrity

Seal integrity is highly dependent on the following foil characteristics:

1. Heat-Seal Coating Consistency

The coating layer must be uniform and precisely controlled.

Variations can lead to:

  • uneven sealing
  • weak bond areas
  • increased risk of leakage

2. Coating–Substrate Compatibility

The coating formulation must match the forming film or laminate structure.

Incorrect compatibility may result in:

  • poor adhesion
  • seal failure under stress

3. Foil Surface Quality

Surface defects such as pinholes, contamination, or irregularities can compromise sealing.

High-quality foils ensure:

  • clean, defect-free surfaces
  • reliable contact during sealing

4. Barrier Properties

Aluminum foil must provide a strong barrier against:

  • moisture
  • oxygen
  • light

Any compromise in barrier integrity increases product vulnerability.

Seal Integrity Testing from a Material Perspective

While testing is performed at the packaging level, results often reflect material performance.

1. Seal Strength Testing (Blister)

Evaluates the bond quality achieved by the foil coating with the forming film.

2. Peel Strength Testing (Strip Packaging)

Measures the separation force in laminated structures, indicating lamination consistency.

3. Dye Penetration & Leak Testing

Helps identify micro-defects that may originate from:

  • coating inconsistency
  • surface imperfections
  • material variability

These tests are essential for validating both material selection and supplier consistency.

Common Material-Related Causes of Seal Failure

Many seal failures originate from foil-related issues rather than process errors:

  • inconsistent heat-seal coating application
  • poor coating adhesion properties
  • variation between production batches
  • surface contamination or defects
  • inadequate lamination quality (in strip foils)
Selecting a reliable foil supplier with controlled manufacturing processes significantly reduces these risks.

Regulatory Expectations

Regulatory authorities expect pharmaceutical companies to ensure that packaging materials consistently meet defined performance standards.

This includes:

  • qualification of packaging materials
  • validation of sealing performance
  • documentation of material specifications

Foil quality, coating consistency, and supplier reliability are therefore critical components of regulatory compliance.

Role of High-Quality Foils in Packaging Reliability

Consistent seal integrity is not achieved by process control alone—it requires high-quality, precisely engineered aluminum foils.

Pharmaceutical-grade foils should offer:

  • uniform heat-seal coating
  • reliable bonding performance
  • excellent barrier protection
  • batch-to-batch consistency

These attributes enable stable sealing performance across high-speed production lines and global supply chains.

Strengthening Seal Integrity Through Material Excellence

Seal integrity is a fundamental requirement in pharmaceutical packaging. While sealing parameters and equipment play a role, material quality—especially aluminum foil performance—is a primary driver of reliability.

By selecting the right foil structures, ensuring coating compatibility, and maintaining strict quality standards, manufacturers can significantly reduce packaging risks.

Strong seal integrity helps:

  • protect product stability
  • minimize recalls and complaints
  • meet global regulatory requirements
  • ensure patient safety

Sanwariya Packaging supports these outcomes by supplying pharmaceutical aluminum foils designed for consistent coating performance, reliable sealing compatibility, and high barrier protection. With controlled manufacturing processes and strict quality standards, Sanwariya Packaging enables pharmaceutical companies to achieve dependable packaging performance at scale.