Blog by Sanwariya Packaging

Your Trusted Partner in Packaging

Learn About Our Vision for the Future And Grow with Us.

Your Trusted Partner in Pharma Packaging

Learn about our vision for the future and grow with us.

Your Trusted Partner
in Pharma Packaging

Learn about our vision for the future and grow with us.

Know More

Category: Anti-Counterfeit Solutions

Counterfeit Drug Trends in LATAM & Africa

Counterfeit medicines remain one of the most serious challenges in global pharmaceutical supply chains. In several emerging markets, including regions across Latin America (LATAM) and Africa, authorities and industry stakeholders continue to monitor rising cases of falsified or diverted medicines entering legitimate distribution channels.

While regulatory frameworks and enforcement efforts are improving, counterfeit products still find entry points through informal markets, parallel supply chains, and weak distribution controls. Because packaging is often the first visible indicator of product authenticity, pharmaceutical companies rely heavily on secure packaging design to detect and prevent manipulation.

Understanding regional counterfeit trends and identifying packaging risk signals are therefore essential for companies supplying medicines to these markets.

Counterfeit Entry Points in Emerging Markets

LATAM and African pharmaceutical markets are expanding rapidly, with increasing demand for both generic and branded medicines. However, the growth of pharmaceutical trade has also created opportunities for counterfeiters to introduce falsified products into distribution networks.

Common entry points include unauthorized wholesalers, unregulated online sales platforms, and informal pharmacy channels. In some cases, diverted products are repackaged or relabeled to mimic legitimate medicines before being reintroduced into the market.

Cross-border trade routes can also complicate monitoring efforts. Medicines may move through multiple countries before reaching the final destination, making it more difficult to trace packaging origins and verify product authenticity.

These challenges highlight the importance of packaging systems that incorporate visible and traceable security elements.

Common Signs of Packaging Manipulation

Counterfeit medicines often attempt to replicate the visual appearance of legitimate packaging. However, subtle differences in packaging quality or structure can reveal potential manipulation.

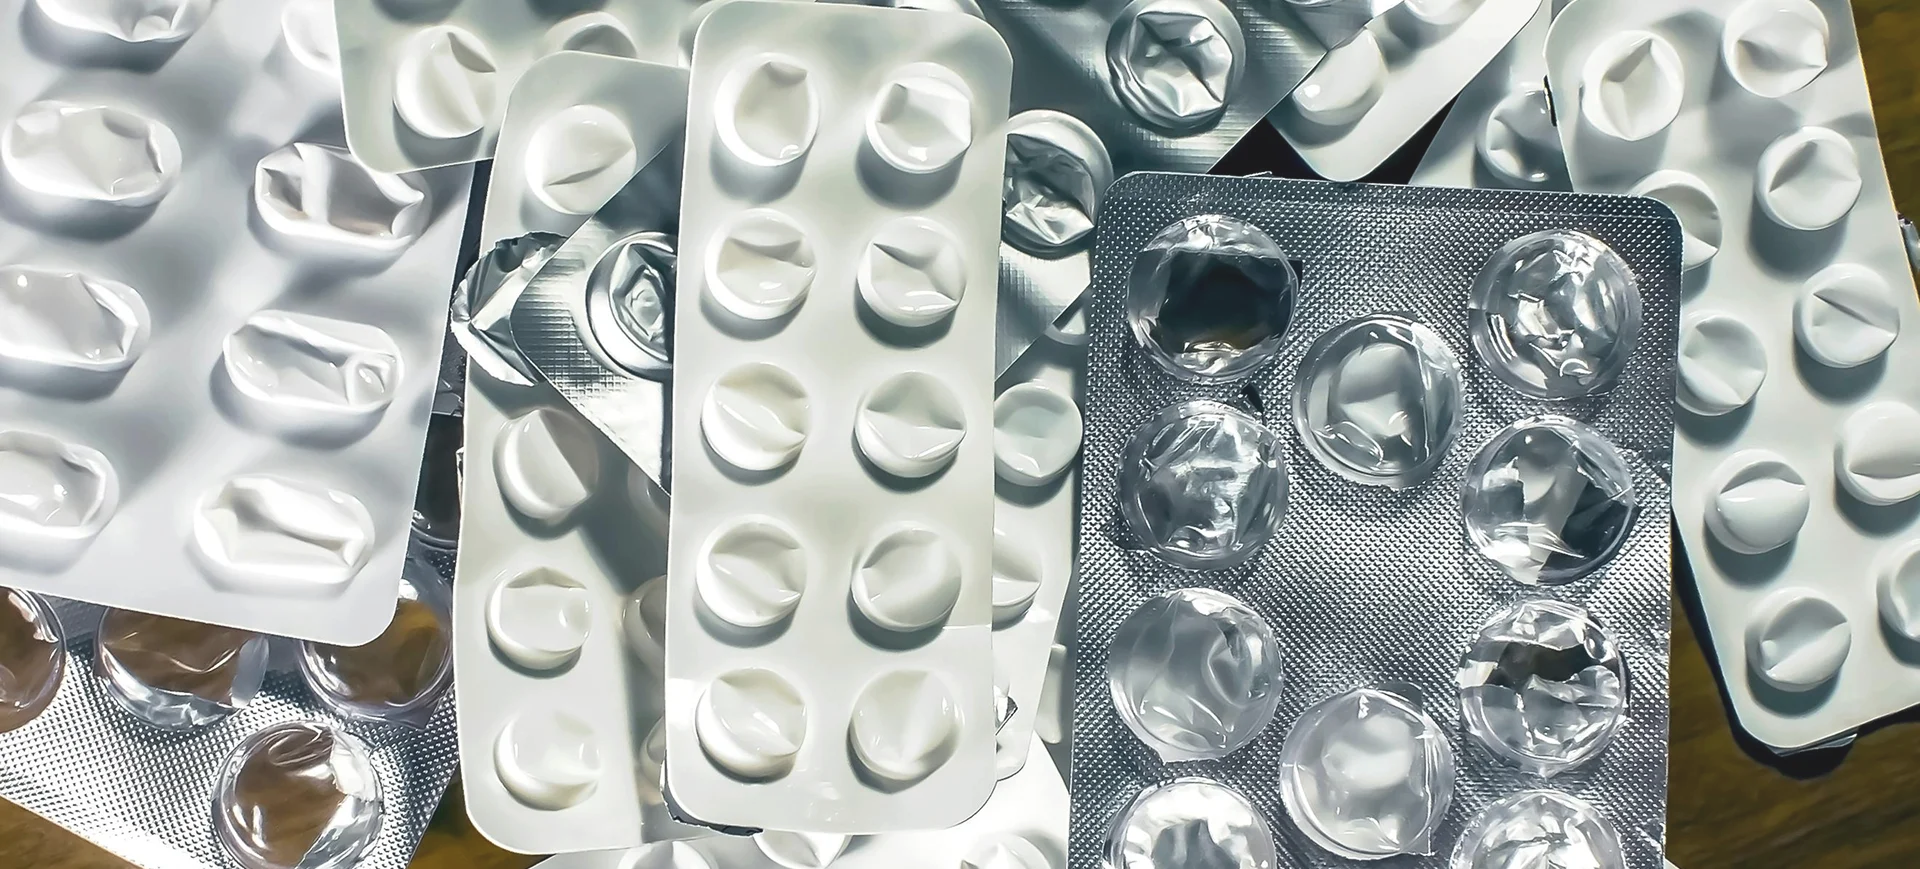
One common signal is irregular blister sealing. Counterfeit operations may use inferior sealing equipment, resulting in inconsistent seal patterns or weakened blister cavities. Packaging edges may appear uneven or slightly distorted.

Another indicator is printing inconsistency. Fonts, batch codes, and ink density may differ from authentic packaging. In some cases, printing alignment may be slightly shifted or blurred due to lower-quality printing equipment.

Blister foil surfaces may also show signs of mechanical tampering. Scratches, partial resealing marks, or unusual foil deformation may indicate that original packaging was opened and reassembled.

Recognizing these signs helps quality teams identify suspicious products during inspections.

Security Printing Features in Pharmaceutical Packaging

To combat counterfeit risks, pharmaceutical companies increasingly integrate security printing technologies into packaging materials. These features allow both regulators and supply chain partners to verify product authenticity more easily.

Security elements may include microtext printing, special inks that change color under different lighting conditions, and unique batch coding systems. Some packaging also incorporates serialized data that can be verified through digital tracking platforms.

Blister foil printing can support these security measures by maintaining consistent print quality and clear code visibility. Stable ink adhesion and precise printing help ensure that security elements remain readable throughout the product lifecycle.

When combined with proper supply chain monitoring, these features strengthen protection against counterfeit manipulation.

The Role of Tamper-Evident Packaging

Tamper-evident packaging plays a critical role in identifying potential product interference. Blister packaging naturally provides some level of tamper visibility because each cavity must be punctured to remove the medicine.

However, additional security cues can further strengthen packaging protection. For example, specialized foil coatings or structural features may reveal visible damage if someone attempts to peel or reseal blister packs.

Clear evidence of tampering allows pharmacists, distributors, and regulators to detect suspicious products before they reach patients.

By integrating tamper-evident design principles, pharmaceutical companies reduce the likelihood that counterfeit products can be successfully reintroduced into legitimate supply chains.

Monitoring Counterfeit Risk Through Packaging

Companies distributing medicines in LATAM and African markets often work closely with regulatory authorities and brand protection teams to monitor counterfeit risks. Packaging plays an important role in these monitoring strategies.

Quality teams may track packaging complaints, review returned products, and analyze suspicious packaging samples to identify patterns of counterfeit activity. These investigations help companies refine packaging specifications and improve security features over time.

In addition, supplier qualification and strict packaging material controls help ensure that authorized packaging components remain traceable and consistent across production batches.

These practices contribute to stronger product protection throughout international supply chains.

Strengthening Packaging Protection Against Counterfeits

Counterfeit medicines pose serious risks to patient safety and brand integrity. As pharmaceutical companies expand distribution across LATAM and African markets, monitoring packaging vulnerabilities and implementing effective security measures becomes increasingly important.

By incorporating secure printing techniques, tamper-evident structures, and consistent packaging quality, pharmaceutical manufacturers can significantly reduce the risk of counterfeit manipulation. Packaging systems designed with strong barrier integrity and reliable printing performance support both product protection and supply chain transparency.

Sanwariya Packaging manufactures pharmaceutical aluminum foils designed to support stable printing performance, clear batch coding visibility, and reliable sealing integrity for blister packaging applications. Through advanced manufacturing processes and strict quality controls, Sanwariya Packaging supports pharmaceutical companies in developing secure packaging solutions that help protect medicines across global markets.

Counterfiet_medcines

Counterfeit medicines in Egypt are a supply-chain problem, a regulatory problem and a packaging problem all at once. When a falsified product reaches a pharmacy shelf, it can pass for a genuine medicine to almost everyone who handles it. That makes packaging the first thing a counterfeiter copies and the first thing a brand owner must be able to defend.

For pharmaceutical manufacturers, brand owners and regulatory teams, the question is how to make genuine packaging harder to imitate and easier to verify, not only how to detect fakes after the fact.

This blog explains the counterfeit landscape in Egypt, how falsified products enter pharmaceutical supply chains, where packaging is vulnerable, and how secure foil and product identification fit into a broader anti-counterfeit strategy.

Counterfeit medicines in Egypt are best addressed through layered protection: secure primary packaging such as hologram and printed foils, serialization and track-and-trace, controlled distribution, and verification tools that pharmacists and patients can actually use.

Understanding the Counterfeit Medicine Landscape in Egypt

Counterfeit or falsified medicines are products that deliberately misrepresent their identity, composition or source. They may contain no active ingredient, the wrong dose, a different ingredient, or harmful contaminants, while carrying the name and appearance of a trusted brand.

The World Health Organization estimates that at least 1 in 10 medicines in low- and middle-income countries are substandard or falsified. This is an estimate for low- and middle-income countries and should not be interpreted as an Egypt-specific statistic. This is a global or regional estimate and should not be interpreted as an Egypt-specific statistic. Egypt, like other markets with complex pharmaceutical supply chains, continues to strengthen systems designed to improve product identification, traceability and regulatory oversight.

Egypt has also strengthened pharmaceutical traceability through the Egyptian Track & Trace System (EPTTS), overseen by the Egyptian Drug Authority (EDA). Under the Phase 1 technical requirements published in 2026, serialization is mandatory at the secondary-packaging level, with EPTTS requiring a Data Matrix ECC 200 containing key product information such as GTIN, serial number, expiry date and batch/lot. Manufacturers and exporters should verify the latest EDA requirements before finalizing packaging artwork, serialization workflows or security features.

Common risk categories in markets like Egypt include:

  • High-demand chronic and lifestyle medicines
  • Products affected by shortages or price gaps
  • Medicines sold through informal or unverified channels
  • Brands with strong reputations and visible packaging

How Counterfeit Products Enter Pharmaceutical Supply Chains

Counterfeit products rarely arrive through one obvious door. They typically enter wherever visibility is lowest.

Common entry points include:

  • Unauthorized or unlicensed distributors and intermediaries
  • Parallel trade and repackaging outside controlled channels
  • Diversion and re-entry of genuine, expired or returned stock
  • Online sales and informal retail outlets
  • Cross-border movement through less-monitored routes

The longer and more fragmented the supply chain, the more handover points exist where a falsified pack can be swapped in. This is why supply-chain transparency and packaging security have to work together.

Packaging Vulnerabilities That Can Enable Imitation

Counterfeiters are not copying the medicine first. They are copying what people see and trust: the carton, the blister card and the printed foil. Packaging that is easy to reproduce is easy to fake.

Typical packaging vulnerabilities include:

  • Standard printed foil with no unique security feature
  • Simple printing that can be replicated with commercial equipment
  • Cartons and leaflets that can be reproduced more easily than primary packaging
  • Absence of covert or machine-readable identifiers
  • Unclear visual cues that pharmacists and patients cannot easily check

The closer a security feature sits to the medicine itself, the harder it is to remove, reuse or convincingly imitate.

This is why primary packaging, especially the blister foil that directly seals each dose, is an important place to add protection. A carton can be replaced. A foil that carries integrated security features is far harder to duplicate.

Why Authentication and Product Identification Matter

Protection only works if someone can check it. Authentication turns packaging from a passive container into an active line of defense.

Effective authentication generally combines several layers:

  • Overt features: visible to the naked eye, such as holograms and distinctive foil patterns, for quick checks by pharmacists and patients
  • Covert features: hidden marks or inks that trained inspectors or tools can verify
  • Digital identifiers: serialized identifiers such as 2D Data Matrix codes, which can connect individual packs with traceability systems and product information.
  • Batch-level traceability: consistent batch, manufacturing and expiry information that can be cross-checked
A pack that can be identified, traced and verified gives regulators, distributors and patients something concrete to rely on, and gives brand owners evidence when a suspect product is found.

Regulatory and Supply-Chain Considerations

Packaging decisions for the Egyptian market should be made with regulators and the supply chain in mind, not just the artwork team.

Key considerations for manufacturers and exporters include:

  • Alignment with current EDA registration, labeling and EPTTS serialization requirements, including applicable secondary-packaging identification requirements
  • Compatibility of security features with high-speed blister packaging lines
  • Consistent artwork control, including Arabic and multilingual text requirements
  • Documented supplier qualification and quality agreements for packaging materials
  • Coordination between packaging, regulatory, QA/QC and supply-chain teams

Security features must also be practical. A feature that disrupts sealing performance, print registration or line speed will not survive production, however impressive it looks.

The Role of Secure Packaging in a Broader Anti-Counterfeit Strategy

No single feature stops counterfeiting. Secure packaging is one layer in a wider strategy that also includes serialization, distributor control, market surveillance, staff training and cooperation with authorities.

Where packaging contributes most:

  • Deterrence: advanced foil features raise the cost and difficulty of copying
  • Detection: overt and covert features give inspectors and pharmacists a fast way to spot suspect products
  • Protection of integrity: strong, consistent foil structures keep the medicine protected until the moment of use
  • Brand confidence: visible security reassures healthcare professionals and patients
The most effective approach layers these features so that a counterfeiter would have to defeat several at once.

How Sanwariya Packaging Supports Anti-Counterfeit Strategies

Sanwariya Packaging is a manufacturer and exporter of pharmaceutical aluminum foils, both unprinted and printed, built for reliable barrier performance, consistent sealing and stable print quality.

For brand owners concerned about imitation, relevant options include:

Through controlled manufacturing and strict quality processes, Sanwariya works with pharmaceutical companies to develop foil solutions that combine protection, printability and security for demanding export markets.

Ready to strengthen your packaging against counterfeiting? Get in touch with our team or request a quote.

Related Blogs

Proper handling, storage, and transport of pharma foil

Pharmaceutical products distributed internationally must comply with labeling regulations across multiple countries. In many markets, medicines are required to display information in more than one language to ensure that patients and healthcare professionals clearly understand product details and usage instructions. 

As a result, pharmaceutical packaging often needs to accommodate multilingual text while maintaining readability, regulatory compliance, and accurate information presentation. Printed aluminum blister foils frequently carry important product information such as medicine names, dosage strengths, batch details, manufacturing information, and storage instructions. 

When these details must appear in multiple languages, careful layout design becomes essential. Font size, text spacing, line order, and translation accuracy must all be managed to ensure that information remains clear and compliant. 

This blog explains how pharmaceutical companies design foil text layouts for multilingual export markets and highlights the importance of font selection, regulatory text structure, and error-free translations in multilingual pharma foil printing.

Why Multilingual Packaging Is Required in Global Markets

Pharmaceutical companies exporting medicines to international markets must follow the labeling requirements established by local regulatory authorities. Many regions require medicines to display product information in multiple languages to support safe usage and patient understanding.

Multilingual packaging helps ensure that essential product information is accessible to a diverse population.

Common reasons for multilingual labeling include:

  • Regulatory requirements in multilingual regions
  • Patient safety and accessibility considerations
  • Clear communication for healthcare professionals
  • Standardized labeling across export markets

Countries or regions with multiple official languages often require bilingual or multilingual labeling to ensure that product information is understood by all users.

When blister foils contain printed product information, the layout must accommodate these language requirements without compromising readability.

Challenges of Multilingual Text on Blister Foils

Blister foils have limited printable space, especially when compared with outer cartons or patient information leaflets. This limited surface area makes multilingual layout design more complex.

Adding multiple languages to the same foil requires careful planning to ensure that each line of text remains readable and correctly aligned.

Common challenges include:

  • Limited space for multiple language blocks
  • Variations in word length between languages
  • Maintaining clear spacing between text lines
  • Preserving readability on small blister cavities
Packaging development teams must design layouts that balance space constraints with regulatory labeling requirements. Proper planning during the artwork stage helps prevent overcrowded or difficult-to-read packaging.

Font Size and Spacing Considerations

Maintaining readable text is one of the most important aspects of multilingual pharmaceutical labeling. Font sizes must be large enough to remain legible while still fitting within the available print area on the foil.

Several design considerations help maintain readability:

  • Consistent font sizes across languages
  • Adequate spacing between lines of text
  • Clear separation between language sections
  • Avoidance of overly condensed fonts
Spacing becomes particularly important when multiple languages appear on a single foil surface. If text is too closely spaced, it may become difficult to read after printing or during product handling. Packaging artwork teams therefore evaluate layout designs carefully before finalizing the print artwork.

Regulatory Line Order and Information Hierarchy

Regulatory guidelines often specify the order in which certain information must appear on pharmaceutical packaging. This includes elements such as the product name, dosage strength, manufacturing details, batch number, and expiration date.

When designing multilingual layouts, the structure of this information must remain consistent across all languages.

Typical layout considerations may include:

  • Placing critical product identification details in a prominent position
  • Maintaining the same information sequence across languages
  • Ensuring regulatory text remains clearly visible
  • Avoiding overlap between different language blocks

Maintaining a logical information hierarchy helps ensure that healthcare professionals and patients can quickly identify important product details.

Packaging designs must therefore balance regulatory structure with available print space.

Preventing Translation Errors in Packaging Artwork

Accurate translation is essential when pharmaceutical packaging is printed in multiple languages. Even small translation errors can create confusion or lead to regulatory compliance issues.

To prevent such risks, pharmaceutical companies often follow structured translation verification processes.

These processes may include:

  • Professional medical translation services
  • Review by regulatory or medical specialists
  • Cross-checking translations against approved product documentation
  • Final proofreading before artwork approval

Because blister foils are printed in large production volumes, translation accuracy must be confirmed before printing begins.

Correcting errors after production can result in material waste or packaging delays.

Printing Precision and Layout Stability

Printing multilingual text on aluminum foil requires precise alignment and consistent print quality. Small variations in print registration or layout alignment may affect text readability, especially when multiple language blocks appear close together.

Production teams monitor several factors to maintain layout accuracy:

  • Precise printing registration across foil reels
  • Stable ink density for small text characters
  • Controlled printing pressure to maintain clarity
  • Consistent alignment of repeated blister patterns

Maintaining stable printing conditions ensures that multilingual text remains clear and readable across the entire production batch.

Reliable printing processes are therefore essential for high-quality multilingual pharma foil printing.

Export Market Considerations for Multilingual Packaging

Pharmaceutical companies supplying medicines to multiple regions often manage several packaging variations to meet local language requirements.

Export teams work closely with packaging and regulatory departments to ensure that each market receives compliant packaging.

Important considerations for export packaging may include:

  • Adapting packaging artwork for region-specific language requirements
  • Ensuring translations meet local regulatory guidelines
  • Managing multiple artwork versions for different markets
  • Maintaining consistency across packaging materials

These processes help ensure that medicines distributed internationally meet both regulatory expectations and patient communication needs.

Supporting Clear Communication Across Global Markets

Multilingual pharmaceutical packaging plays an important role in ensuring that medicine information is accessible to patients and healthcare professionals around the world. Designing foil text layouts for multiple languages requires careful attention to font sizing, spacing, information hierarchy, and translation accuracy.

By following structured artwork design practices and maintaining precise printing control, pharmaceutical companies can produce packaging that remains clear, compliant, and easy to read across international markets.

Effective multilingual labeling helps reduce communication barriers and supports safe medicine use in diverse healthcare environments.

Sanwariya Packaging manufactures printed pharmaceutical aluminum foils designed to support precise text reproduction, consistent print alignment, and high-quality multilingual printing. Through advanced printing capabilities and controlled production processes, Sanwariya Packaging helps pharmaceutical companies deliver packaging solutions that maintain clarity and regulatory compliance across global export markets.

Serialization updates for printed foils in 2026

Medicines are carefully formulated to remain stable and effective throughout their shelf life. However, some pharmaceutical compounds are highly sensitive to light, particularly ultraviolet (UV) radiation. When exposed to light, these medicines may undergo chemical degradation that reduces potency or alters their safety profile.

Because of this risk, protecting medicines from light exposure is an important consideration during pharmaceutical packaging design. Packaging materials must shield sensitive formulations from harmful wavelengths while maintaining stability during storage, transportation, and distribution.

Blister packaging using aluminum-based foils plays a significant role in protecting light-sensitive medicines. The reflective properties of aluminum, combined with specialized coatings, help prevent ultraviolet radiation from reaching the drug product.

This blog explains the science of UV degradation, how aluminum foil provides light protection, the testing methods used to validate UV resistance, and how pharmaceutical companies select the most appropriate foil structures for light-sensitive medicines.

Why Light Exposure Can Damage Medicines

Many pharmaceutical ingredients are sensitive to electromagnetic radiation within the ultraviolet and visible light spectrum. When exposed to light, the energy absorbed by the molecule can trigger chemical reactions that alter the structure of the active ingredient.

These reactions may lead to several types of degradation.

  • Loss of drug potency
  • Formation of degradation by-products
  • Color changes in the formulation
  • Reduced shelf life or stability

Certain categories of medicines are particularly vulnerable to photodegradation. These may include antibiotics, vitamins, biological compounds, and formulations containing complex organic molecules.

Even limited exposure during transportation or storage can contribute to gradual degradation if packaging does not provide adequate protection.

For this reason, stability studies often include light exposure testing to determine whether protective packaging is required.

Understanding UV Degradation in Pharmaceutical Stability

Photodegradation occurs when molecules absorb photons from light energy. Ultraviolet radiation carries higher energy compared with visible light, making it especially capable of breaking chemical bonds.

In pharmaceutical stability studies, exposure to light can cause molecular reactions such as oxidation, isomerization, or structural breakdown of active ingredients.

The likelihood of degradation depends on several factors.

  • Wavelength of the incoming light
  • Duration of exposure
  • Sensitivity of the drug molecule
  • Transparency of the packaging material

Packaging materials that allow UV light to pass through may expose the product to degradation risks over time. As a result, selecting materials with strong UV-blocking properties is an important part of packaging development for light-sensitive medicines.

How Aluminum Foil Acts as a UV Barrier

Aluminum foil provides one of the most effective barriers against light exposure in pharmaceutical packaging. Unlike transparent or translucent materials, aluminum reflects and blocks a large portion of incoming radiation.

The metal surface reflects both visible and ultraviolet wavelengths, preventing light from reaching the medicine inside the blister cavity.

This reflective behavior provides several advantages.

  • Near-complete opacity to light
  • Strong UV blocking capability
  • Stable protection across different wavelengths
  • Consistent performance during storage and transport

Because of these properties, aluminum foil is widely used in blister foils for light-sensitive formulations.

When combined with appropriate coatings and printing layers, foil structures can maintain both functional protection and regulatory labeling requirements.

Reflectivity Advantage of Aluminum in Pharmaceutical Packaging

The reflective surface of aluminum plays a key role in reducing UV penetration. When ultraviolet radiation strikes the foil surface, a significant portion of the energy is reflected away instead of passing through the material.

This reflective behavior helps maintain a stable internal environment for the medicine.

The performance of the foil barrier can be influenced by factors such as:

  • Foil thickness
  • Coating layers applied to the surface
  • Printing inks and pigments
  • Surface finish of the foil

Higher-quality foil structures maintain consistent reflectivity while also supporting reliable printing and sealing performance.

This combination of mechanical strength and optical protection makes aluminum foil particularly suitable for medicines that require strict light protection, including advanced structures like cold forming foils and multi-layer foils.

Testing Light Protection in Pharmaceutical Packaging

Pharmaceutical companies must demonstrate that packaging materials adequately protect light-sensitive medicines throughout the product’s shelf life.

This evaluation is typically performed during stability testing under controlled laboratory conditions.

Common testing approaches include:

  • Exposure to defined ultraviolet and visible light levels
  • Accelerated stability testing with controlled light sources
  • Measurement of degradation products after exposure
  • Comparison of protected and unprotected samples

International stability guidelines often define the total light exposure conditions required for photostability testing.

These tests help determine whether the selected packaging structure provides sufficient UV protection for the medicine.

If degradation is observed, packaging engineers may modify the material structure or increase the protective barrier properties.

Selecting the Right Foil Coating for UV Protection

While aluminum itself provides strong light protection, coatings and printing layers applied to the foil can influence overall performance.

Coatings are often applied to support sealing, printing, or machine compatibility. However, these coatings must also maintain the protective characteristics of the foil.

Packaging development teams evaluate several coating-related factors.

  • Compatibility with blister sealing processes
  • Resistance to environmental exposure
  • Stability of printed graphics during storage
  • Maintenance of UV-blocking performance

Specialized coatings may also reduce surface reflections that could interfere with printing or scanning technologies while maintaining the underlying barrier performance.

Selecting the correct coating system ensures that the foil continues to provide effective UV protection throughout the product lifecycle.

Challenges When Shipping Light-Sensitive Medicines Globally

Medicines distributed internationally may encounter a wide range of environmental conditions during transportation. Products shipped to regions with strong sunlight or high ambient temperatures may experience greater light exposure during handling and storage.

Export-oriented pharmaceutical companies therefore evaluate packaging carefully when shipping to high-exposure markets.

Potential risks during distribution include:

  • Prolonged exposure to sunlight during logistics handling
  • Storage in brightly lit warehouse environments
  • Transportation through regions with intense solar radiation

Using packaging materials with strong light barrier properties helps reduce these risks and ensures that medicines remain stable until they reach patients.

Regulatory Expectations for Photostability Protection

Global pharmaceutical regulators expect companies to demonstrate that packaging materials adequately protect medicines from environmental factors such as light, moisture, and oxygen.

Photostability studies form part of the broader stability testing framework used to establish shelf life.

Regulatory documentation may include:

  • Photostability study reports
  • Packaging material specifications
  • Validation of protective packaging performance
  • Long-term stability data under recommended storage conditions

Maintaining thorough documentation helps ensure compliance during regulatory submissions and inspections.

Packaging materials must therefore be selected not only for functional performance but also for their ability to support documented stability outcomes.

Ensuring Stability for Light-Sensitive Medicines

Protecting medicines from ultraviolet radiation is an essential aspect of pharmaceutical packaging design. Exposure to light can cause chemical degradation that affects both product efficacy and safety.

Aluminum blister foils provide an effective solution by reflecting and blocking ultraviolet radiation before it reaches the medicine. When combined with appropriate coatings and carefully designed packaging structures, these materials help maintain stability throughout the product’s lifecycle.

For pharmaceutical companies developing light-sensitive formulations, selecting the right packaging materials is a critical step in ensuring long-term product quality and regulatory compliance.

Sanwariya Packaging manufactures pharmaceutical aluminum foils designed to provide strong barrier protection, reliable printing performance, and compatibility with modern blister packaging systems. Through controlled manufacturing processes and advanced capabilities supported by its infrastructure, Sanwariya Packaging supports pharmaceutical companies in developing packaging solutions that help protect sensitive medicines throughout global distribution.For further discussions or requirements, you can get in touch with us or directly request a quote.

Choosing optimal foil for high-sensitivity pharmaceutical products

High-sensitivity pharmaceutical formulations require more than standard packaging protection. Even very small exposure to moisture, oxygen or light can directly affect product stability, shelf life and regulatory acceptance.

In real manufacturing and distribution environments, issues such as unexpected degradation, impurity growth, stability failures or reduced shelf life are frequently traced back to one root cause: inadequate barrier performance of the pharmaceutical packaging material.

This is where high barrier pharma foil becomes a critical packaging decision.

This blog explains, in practical terms, how sensitive formulations should be matched with the right foil structure, how packaging influences stability risk, and how pharmaceutical teams can select high-barrier foils with confidence for regulated and export markets.

What makes a formulation highly sensitive

A formulation is considered high-sensitivity when very small environmental exposure can trigger measurable quality changes.

Typical examples include:

1. Moisture-sensitive formulations

Hygroscopic APIs, effervescent tablets, dispersible tablets and low-dose products. Even brief humidity exposure can cause softening, dissolution failures or hydrolytic degradation, making the use of blister foils and strip laminated foils critical for moisture protection.

2. Light-sensitive formulations

Photo-unstable APIs, hormonal products and certain antibiotics, where light exposure can reduce potency before expiry, often requiring cold forming foils and specialized multi-layer foils for complete light barrier.

3. Oxygen-sensitive formulations

APIs prone to oxidation, leading to impurity growth, color changes and assay drift, where high-integrity pharmaceutical packaging becomes essential.

4. Low-dose and high-potency formulations

Minor degradation becomes critical for content uniformity and regulatory compliance, making advanced multi-layer foils an important protective option.

For these products, packaging is not passive. It directly controls the stability risk profile.

Why high barrier pharma foil becomes necessary

Standard foil structures provide general protection. However, for sensitive products, moderate barrier performance is often insufficient over long storage periods and international distribution of finished medicines packed using pharmaceutical products.

High barrier pharma foil is designed to provide:

  • very low moisture transmission
  • complete light protection
  • very low oxygen permeation
  • consistent barrier performance throughout shelf life

In practical terms, the aluminium layer delivers the primary barrier, while coating and seal layers protect the aluminium and maintain barrier integrity during forming, sealing and handling in modern pharmaceutical packaging operations.

Stability risks that packaging must control

For sensitive formulations, the main environmental risks are:

  • moisture ingress
  • light exposure
  • oxygen permeation
  • long storage and transit cycles
These risks increase significantly in Climatic Zones III and IV, where high humidity and temperature exposure are common. In such markets, selecting high-barrier packaging formats such as cold forming foils is a preventive stability measure.

How foil structure determines real barrier performance

Pharmaceutical foil is a multi-layer structure. Each layer plays a defined functional role.

A typical high-barrier foil structure includes:

  • aluminium foil as the primary barrier
  • protective coatings or lacquers
  • functional sealant layers

A well-engineered structure slows moisture and gas migration at multiple interfaces. A weak or incompatible structure allows penetration pathways to form, even when aluminium thickness appears adequate, which is why engineered multi-layer foils are widely used for sensitive medicines.

Key insight:
Two foils with similar thickness can show very different barrier performance because protection depends on structural integrity, not thickness alone.

How individual foil layers support sensitive drug protection

  • Aluminium layer – the primary barrier: Provides moisture, oxygen and light protection. Pinhole control and thickness consistency are critical for long-term stability in formats such as blister foils and strip laminated foils.
  • Coatings and lacquers – barrier durability: Protect aluminium during forming and handling, reduce micro-crack formation and support durability under prolonged humidity exposure, especially in complex pharmaceutical packaging applications.
  • Sealant layers – the most frequent weak point: Create the final protective seal and directly influence moisture ingress at the seal interface. Many real-world failures originate at the seal area rather than through the aluminium itself.

Standard foil versus high-barrier foil

AspectStandard foil structureHigh-barrier foil structure
Moisture resistanceModerateVery high
Long-term stabilityLimited in humid conditionsConsistent across climates
Suitability for exportsShort or controlled routesLong and high-risk distribution routes
Regulatory confidenceConditionalStrong and data-driven

High-barrier structures are designed to perform reliably under sustained environmental stress, not only during short laboratory testing periods.

When high-barrier foil becomes essential

High-barrier pharmaceutical foils become necessary when:

  • the formulation is moisture- or light-sensitive
  • shelf life exceeds 24 months
  • distribution includes Climatic Zones III and IV
  • long transit, port storage or uncontrolled warehousing is expected
In many export markets across Asia, Africa and Latin America, standard foil structures may pass early stability studies but fail under real storage conditions when using conventional PVC foils without enhanced barrier layers.

What quality and regulatory teams expect

Barrier performance must be demonstrated and documented.

For sensitive formulations, packaging qualification typically includes:

  • validated moisture and oxygen transmission testing
  • stability studies aligned with the intended climatic zones
  • seal integrity and ageing evaluations
This data supports packaging approval during registration, export readiness and shelf-life commitments.

Common real-world failures linked to incorrect foil selection

Across domestic and export markets, similar patterns are repeatedly observed:

  • stability passes initially but fails after prolonged humid storage
  • tablets soften, stick or discolour before expiry
  • market complaints occur despite compliant formulations
  • costly revalidation follows post-approval packaging changes
In most cases, the root cause is not formulation design, but barrier performance that was underestimated during foil selection of inappropriate pharmaceutical products.

A practical selection checklist for sensitive formulations

Before finalizing a foil grade, confirm:

  • the formulation’s sensitivity to moisture, light and oxygen
  • the climatic zones the product will encounter
  • the full storage and transit duration
  • seal layer compatibility with the forming material
  • availability of validated barrier and stability data

Selecting high barrier pharma foil should be treated as a preventive quality decision, not a corrective action.

For high-sensitivity medicines, packaging performance directly defines product stability.

High-barrier pharmaceutical foil plays a decisive role in:

  • moisture and light protection
  • shelf-life reliability
  • export success
  • regulatory confidence

At Sanwariya Packaging, high-barrier pharmaceutical aluminium foils are developed as stability-driven and compliance-ready solutions for moisture- and light-sensitive medicines—supporting pharmaceutical manufacturers in protecting product quality throughout the entire lifecycle.