Blog by Sanwariya Packaging

Your Trusted Partner in Packaging

Learn About Our Vision for the Future And Grow with Us.

Your Trusted Partner in Pharma Packaging

Learn about our vision for the future and grow with us.

Your Trusted Partner
in Pharma Packaging

Learn about our vision for the future and grow with us.

Know More

Tag: alu-alu foil

Importance of strong foil in pharmacy dispensing

Modern pharmaceutical supply chains often extend across continents. Medicines manufactured in one country may travel thousands of kilometers before reaching distributors, pharmacies, and ultimately patients. During this journey, pharmaceutical products may face fluctuating temperatures, high humidity levels, mechanical stress, and prolonged storage conditions.

For formulations containing sensitive Active Pharmaceutical Ingredients (APIs), these environmental factors can pose significant stability risks. As a result, packaging plays a critical role in maintaining product quality throughout global logistics networks. Selecting the correct blister foil structure helps ensure that medicines remain safe, effective, and stable even after long transit periods.

Why Long Supply Chains Create Stability Challenges

Unlike many consumer products, pharmaceutical medicines must maintain strict quality and stability parameters from manufacturing to patient use. Long-distance transportation introduces multiple stages where environmental conditions may vary.

Shipments frequently move through trucks, shipping containers, cargo aircraft, and distribution warehouses. At each stage, exposure to temperature variation, humidity, and mechanical vibration can occur. Over time, these environmental stresses may affect both the packaging and the product inside.

For APIs that are sensitive to moisture, oxygen, or light, inadequate packaging protection can increase the risk of degradation during transit. Therefore,  pharmaceutical packaging must be designed not only for storage stability but also for real-world supply chain conditions.

Supply Chain Journey Conditions

International pharmaceutical distribution often involves complex logistics routes. A single shipment may move through several countries, climate zones, and transportation modes before reaching the final destination.

Sea freight, which is commonly used for global pharmaceutical distribution, can take several weeks depending on the route. During this period, containers may experience high humidity levels, especially when traveling through tropical or coastal regions.

In addition to environmental exposure, products may also remain in temporary storage at ports, warehouses, and customs facilities. These extended holding periods increase the importance of packaging materials that can maintain strong barrier performance over time.

Understanding the complete supply chain journey helps packaging teams select materials capable of protecting pharmaceutical products during prolonged logistics timelines.

The Role of Humidity Protection

Humidity is one of the most significant environmental threats to pharmaceutical stability during long-distance transportation. Many APIs are sensitive to moisture and can undergo hydrolysis reactions when exposed to elevated humidity levels.

Even small amounts of water vapor entering blister cavities can gradually affect product stability over extended transit periods. High humidity environments combined with long shipping durations can accelerate degradation processes if packaging barriers are insufficient.

High-barrier aluminum blister foils significantly reduce moisture vapor transmission, helping protect the internal environment of each blister cavity. By maintaining a stable microenvironment around the medicine, these barrier materials play a crucial role in preserving API integrity during international shipping.

Mechanical Stress During Transportation

Pharmaceutical products encounter repeated handling throughout the supply chain. Cartons are stacked on pallets, transported by trucks, transferred between warehouses, and loaded onto ships or aircraft.

These operations introduce vibrations, compression forces, and occasional impacts that can stress packaging structures. If blister packs lack adequate mechanical strength, cavities may deform or seals may weaken, potentially allowing environmental intrusion.

Durable pharmaceutical foil structures help maintain seal integrity and cavity stability even under challenging logistics conditions. Strong blister materials reduce the likelihood of packaging damage and help ensure that each dose remains properly protected until it reaches the patient.

Selecting the Correct Barrier Structure

Packaging engineers must evaluate several factors when selecting blister foil structures for products intended for long-distance export. The sensitivity of the API, expected transit duration, and environmental conditions along the shipping route all influence packaging requirements.

Standard blister foil structures may be suitable for domestic distribution or short supply chains. However, products shipped across international routes often require enhanced barrier performance.

Aluminum-based blister foils provide excellent protection against moisture, oxygen, and light. These materials are commonly used for formulations that require high levels of environmental protection during storage and transportation.

By aligning packaging design with logistics realities, pharmaceutical companies can significantly reduce the risk of stability issues during transit.

Packaging Considerations for Export Markets

Global pharmaceutical distribution requires careful coordination between formulation scientists, packaging development teams, and supply chain specialists. Export markets may present environmental conditions that differ significantly from domestic storage environments.

Certain regions experience consistently high humidity, while others may have extreme seasonal temperatures. These environmental variations must be considered when qualifying packaging systems for international distribution.

High-barrier blister packaging helps maintain product stability despite these environmental differences. Reliable packaging solutions support consistent medicine quality regardless of how far the product must travel before reaching healthcare providers and patients.

Maintaining API Stability Across Global Supply Chains

Long-distance pharmaceutical distribution exposes medicines to humidity, temperature changes, mechanical vibration, and extended storage timelines. Effective blister packaging plays a critical role in protecting sensitive APIs from these environmental risks during international transportation.

By selecting high-barrier pharmaceutical foil structures with strong moisture protection and mechanical durability, pharmaceutical manufacturers can maintain product stability throughout complex logistics networks. Proper packaging selection helps ensure medicines retain their safety, potency, and quality from manufacturing facilities to patients worldwide.

Sanwariya Packaging manufactures pharmaceutical aluminum foils designed to provide strong moisture barriers, consistent sealing performance, and reliable mechanical stability for blister packaging applications. Through advanced manufacturing processes and strict quality controls, Sanwariya Packaging supports pharmaceutical companies in protecting API stability across long global supply chains and challenging transit environments.

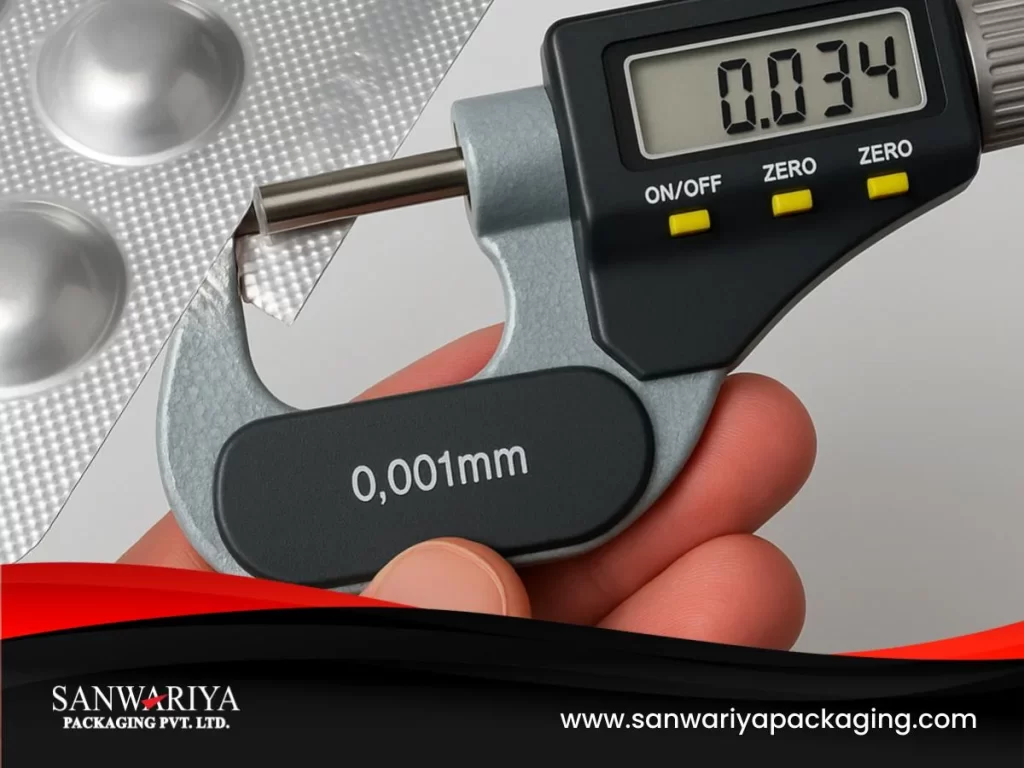
Pharma Foil Thickness & Gauge: What You Need to Know

In pharmaceutical packaging, even the smallest detail can decide whether a medicine reaches patients safe and effective—or fails along the way. According to WHO, packaging-related failures are among the leading causes of drug recalls in developing markets, and one of the most overlooked culprits is foil thickness.

This “micron-level” parameter might seem minor, but it is the backbone of product protection, compliance, and global trust. From shielding medicines against moisture and oxygen to meeting international regulatory standards, foil thickness is a detail every pharma professional—and increasingly, every patient—should understand.

Why Foil Thickness Matters

Pharmaceutical aluminum foil isn’t just a wrapper—it’s a protective barrier. The thickness, measured in microns, directly impacts:

  • Barrier protection – Prevents moisture, light, and oxygen from degrading sensitive medicines.
  • Sealing strength – Ensures blister packs remain leak-proof and tamper-resistant.
  • Shelf life – Preserves drug stability during storage and transport.
Think of it like this: just as a weak lock leaves a door vulnerable, the wrong foil thickness leaves medicines exposed to risks.

Foil Thickness at a Glance

Foil TypeTypical Thickness (Microns)Best Suited ForKey Benefit
Blister Foil (PVC/PVDC + Lidding Foil)20–25 µmStandard tablets & capsulesStrong seal + cost-effective
Alu-Alu Foil (Cold-Form Blister)45–60 µmHighly moisture/light-sensitive drugsMaximum barrier protection
Strip Packaging Foil25–40 µmUnit-dose packaging for tablets/capsulesFlexibility + durability

Quick Tip: In tropical or high-humidity markets, regulators often recommend using the higher end of thickness ranges to ensure drug stability.

Global Standards and Compliance

International regulators such as the FDA, EMA, and WHO expect foils to meet strict performance tests, including:

  • Moisture transmission rate (MTR)
  • Light protection levels
  • Vacuum leak testing
In simple terms, regulators want proof that foil truly protects medicines against air, light, and humidity for the duration of their shelf life.

The Risks of Getting It Wrong

Choosing the wrong thickness isn’t just a technical error—it can have costly consequences:

  • Too thin: Pinholes, faster drug degradation, failed stability studies, and in tropical markets, even product recalls.
  • Too thick: Higher costs, increased shipment weight, and sustainability challenges, without extra protective benefits.
Case in Point: A leading exporter to Southeast Asia once faced regulatory rejection because blister foils couldn’t withstand humidity. The result? Costly recalls and a damaged reputation with distributors.

Myths vs. Facts

  • Myth: Thicker foil is always better.
    Fact: The right thickness balances protection, cost, and sustainability.
  • Myth: Foil standards are universal.
    Fact: Markets differ—CIS and tropical regions often demand higher-barrier foils than Europe.
  • Myth: Thickness doesn’t impact compliance.
    Fact: Regulators routinely test packaging; non-compliance can delay approvals and shipments

Choosing the Right Thickness

Selecting the correct foil requires collaboration across packaging, QA/QC, and supply chain teams. Key factors include:

  • Formulation type – Moisture- or light-sensitive drugs require stronger barriers.
  • Destination market – High-humidity regions demand higher-gauge foils.
  • Regulatory compliance – Standards differ country by country.
  • Sustainability goals – Lightweight foils can reduce cost and carbon footprint.
This decision requires collaboration between packaging development, QA/QC, and supply chain teams.

Smarter, Greener Foils

The industry is moving toward innovations that go beyond thickness:

  • Lightweight foils – Reducing material use without compromising integrity.
  • Eco-friendly designs – Enhancing recyclability and minimizing waste.
  • Digital integration – Embedding track-and-trace for anti-counterfeit protection.
These trends combine sustainability, compliance, and patient safety—the three pillars shaping the future of pharma packaging.

Foil thickness may seem like a small technical detail, but it is central to pharmaceutical safety, compliance, and global trust. The right gauge ensures protection, prevents costly recalls, and strengthens confidence among regulators, distributors, and patients worldwide.

At Sanwariya Packaging, we help pharma brands choose the right foil specifications—balancing protection, compliance, sustainability, and cost-efficiency—so that medicines remain safe, effective, and trusted across international markets.

Looking to optimize your packaging for global exports?
Our experts can guide you in selecting the right foil thickness for every market.

A Closer Look at Alu-Alu Foil: Myths vs. Facts

In pharmaceutical packaging, some materials stand out for their ability to protect medicines under the harshest conditions. Alu-Alu foil is one such solution, trusted worldwide for packing sensitive drugs. Yet, myths still surround it — from being “too costly” to “only for premium medicines.”

It’s time to separate myths from facts and understand why Alu-Alu foil is increasingly considered the gold standard in pharma packaging.

What is Alu-Alu Foil?

Alu-Alu foil, short for aluminum–aluminum cold-form blister packaging, is created by laminating aluminum with nylon and PVC (or other polymers). Unlike regular PVC blisters, Alu-Alu provides a complete barrier against:

  • Moisture (critical in tropical and humid climates)
  • Oxygen (prevents oxidation and drug degradation)
  • Light (protects light-sensitive formulations)
  • Contaminants (ensures patient safety)

Because of these properties, Alu-Alu foil is widely used for antibiotics, anti-malarials, and other highly sensitive formulations that demand maximum stability.

Common Myths About Alu-Alu Foil

Myth 1: “It’s the same as regular aluminum foil.”

Fact: Standard blisters usually have a PVC base, which allows some moisture or oxygen to pass through. Alu-Alu foil, however, creates a 100% barrier, essential for unstable drugs in challenging climates.

Myth 2: “It’s only for premium medicines.”

Fact: Once seen as premium, Alu-Alu is now common across essential generics, especially in ICH Zone IVa and IVb regions (hot and humid zones like Southeast Asia, Africa, and Latin America). Here, drug stability is non-negotiable.

Myth 3: “It’s not eco-friendly.”

Fact: Sustainability in pharma packaging is advancing. By optimizing foil thickness and improving recyclability, manufacturers are making Alu-Alu more sustainable. Some companies are already piloting recovery systems for laminate recycling.

Myth 4: “It’s too costly without added benefits.”

Fact: While Alu-Alu may have a slightly higher upfront cost, its long-term value is undeniable:

  • Fewer recalls: Prevents costly drug recalls caused by moisture or oxygen damage.
  • Extended stability: Keeps medicines stable for up to 36 months in tropical conditions vs. 12–18 months in PVC blisters.
  • Extended stability: Alu-Alu packs provide superior protection against moisture, oxygen, and light — helping maintain the stability of sensitive formulations even in hot and humid (Zone IV) climates. The actual stability period should be supported by product-specific stability studies and regulatory data, ensuring evidence-based validation. (Source: Click Here)
  • Global compliance: Meets USFDA, EMA, and WHO standards, minimizing export rejections.

The real ROI isn’t just cost — it’s stability, compliance, and brand protection.

The Facts That Matter

  • Superior Barrier Protection: Blocks moisture, oxygen, and light.
  • Global Regulatory Recognition: Approved and recommended by USFDA, EMA, WHO for sensitive formulations.
  • Extended Shelf Life: Preserves stability even in extreme climates.
  • Patient Safety First: Minimizes contamination and dosage risks.
  • Sustainability Gains: Ongoing research into recyclable laminates.

Why Alu-Alu Foil Matters for Pharma Companies

For pharma manufacturers, packaging is not just about containment — it’s about compliance, reputation, and trust. Alu-Alu foil helps companies:

  • Meet global export requirements without risking rejection.
  • Protect brands against counterfeiting when combined with serialization printing.
  • Avoid costly recalls and shipment delays due to weak packaging.
  • Strengthen patient trust by delivering safe, stable medicines every time.

Alu-Alu Foil is more than packaging. It is a future-ready solution for drug safety, regulatory compliance, and brand credibility in global markets. While myths persist, the facts are undeniable: Alu-Alu foil offers unmatched protection, longer shelf life, and safeguards patients as well as pharmaceutical companies.

In a world where drug stability can determine patient health outcomes, Alu-Alu Foil stands as a reliable guardian of quality.

Partnering for Safer Pharma Packaging

At Sanwariya Packaging, we deliver pharma-grade Alu-Alu Foils engineered for the highest barrier protection and global compliance. Our expertise ensures your medicines remain stable, secure, and trusted across diverse markets.

Reach out to our team today to discover how our advanced packaging solutions can help you protect your products and your brand reputation.