Sanwariya Packaging Logo
Loading
Skip to main content

Blog by Sanwariya Packaging

Your Trusted Partner in Pharma Packaging

Learn about our vision for the future and grow with us.

Your Trusted Partner
in Pharma Packaging

Learn about our vision for the future and grow with us.

Know More

Your Trusted Partner in Packaging

Learn About Our Vision for the Future And Grow with Us.

Recent Blogs

Counterfeit Drug Trends in LATAM & Africa

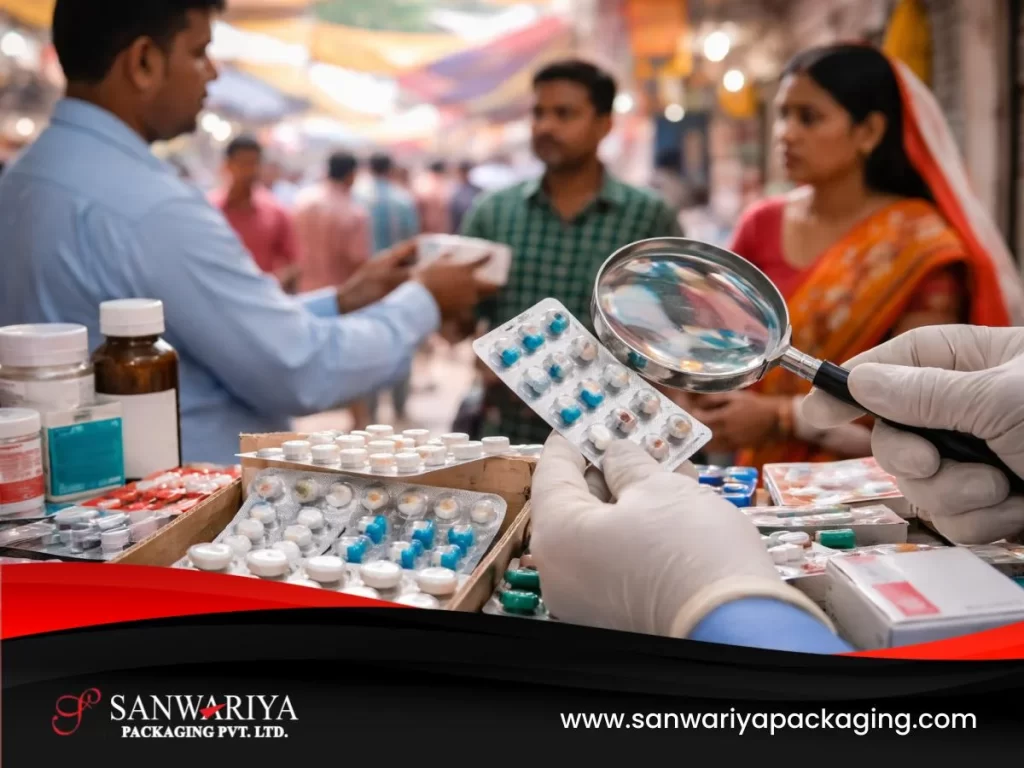
Counterfeit medicines remain one of the most serious challenges in global pharmaceutical supply chains. In several emerging markets, including regions across Latin America (LATAM) and Africa, authorities and industry stakeholders continue to monitor rising cases of falsified or diverted medicines entering legitimate distribution channels.

While regulatory frameworks and enforcement efforts are improving, counterfeit products still find entry points through informal markets, parallel supply chains, and weak distribution controls. Because packaging is often the first visible indicator of product authenticity, pharmaceutical companies rely heavily on secure packaging design to detect and prevent manipulation.

Understanding regional counterfeit trends and identifying packaging risk signals are therefore essential for companies supplying medicines to these markets.

Counterfeit Entry Points in Emerging Markets

LATAM and African pharmaceutical markets are expanding rapidly, with increasing demand for both generic and branded medicines. However, the growth of pharmaceutical trade has also created opportunities for counterfeiters to introduce falsified products into distribution networks.

Common entry points include unauthorized wholesalers, unregulated online sales platforms, and informal pharmacy channels. In some cases, diverted products are repackaged or relabeled to mimic legitimate medicines before being reintroduced into the market.

Cross-border trade routes can also complicate monitoring efforts. Medicines may move through multiple countries before reaching the final destination, making it more difficult to trace packaging origins and verify product authenticity.

These challenges highlight the importance of packaging systems that incorporate visible and traceable security elements.

Common Signs of Packaging Manipulation

Counterfeit medicines often attempt to replicate the visual appearance of legitimate packaging. However, subtle differences in packaging quality or structure can reveal potential manipulation.

One common signal is irregular blister sealing. Counterfeit operations may use inferior sealing equipment, resulting in inconsistent seal patterns or weakened blister cavities. Packaging edges may appear uneven or slightly distorted.

Another indicator is printing inconsistency. Fonts, batch codes, and ink density may differ from authentic packaging. In some cases, printing alignment may be slightly shifted or blurred due to lower-quality printing equipment.

Blister foil surfaces may also show signs of mechanical tampering. Scratches, partial resealing marks, or unusual foil deformation may indicate that original packaging was opened and reassembled.

Recognizing these signs helps quality teams identify suspicious products during inspections.

Security Printing Features in Pharmaceutical Packaging

To combat counterfeit risks, pharmaceutical companies increasingly integrate security printing technologies into packaging materials. These features allow both regulators and supply chain partners to verify product authenticity more easily.

Security elements may include microtext printing, special inks that change color under different lighting conditions, and unique batch coding systems. Some packaging also incorporates serialized data that can be verified through digital tracking platforms.

Blister foil printing can support these security measures by maintaining consistent print quality and clear code visibility. Stable ink adhesion and precise printing help ensure that security elements remain readable throughout the product lifecycle.

When combined with proper supply chain monitoring, these features strengthen protection against counterfeit manipulation.

The Role of Tamper-Evident Packaging

Tamper-evident packaging plays a critical role in identifying potential product interference. Blister packaging naturally provides some level of tamper visibility because each cavity must be punctured to remove the medicine.

However, additional security cues can further strengthen packaging protection. For example, specialized foil coatings or structural features may reveal visible damage if someone attempts to peel or reseal blister packs.

Clear evidence of tampering allows pharmacists, distributors, and regulators to detect suspicious products before they reach patients.

By integrating tamper-evident design principles, pharmaceutical companies reduce the likelihood that counterfeit products can be successfully reintroduced into legitimate supply chains.

Monitoring Counterfeit Risk Through Packaging

Companies distributing medicines in LATAM and African markets often work closely with regulatory authorities and brand protection teams to monitor counterfeit risks. Packaging plays an important role in these monitoring strategies.

Quality teams may track packaging complaints, review returned products, and analyze suspicious packaging samples to identify patterns of counterfeit activity. These investigations help companies refine packaging specifications and improve security features over time.

In addition, supplier qualification and strict packaging material controls help ensure that authorized packaging components remain traceable and consistent across production batches.

These practices contribute to stronger product protection throughout international supply chains.

Strengthening Packaging Protection Against Counterfeits

Counterfeit medicines pose serious risks to patient safety and brand integrity. As pharmaceutical companies expand distribution across LATAM and African markets, monitoring packaging vulnerabilities and implementing effective security measures becomes increasingly important.

By incorporating secure printing techniques, tamper-evident structures, and consistent packaging quality, pharmaceutical manufacturers can significantly reduce the risk of counterfeit manipulation. Packaging systems designed with strong barrier integrity and reliable printing performance support both product protection and supply chain transparency.

Sanwariya Packaging manufactures pharmaceutical aluminum foils designed to support stable printing performance, clear batch coding visibility, and reliable sealing integrity for blister packaging applications. Through advanced manufacturing processes and strict quality controls, Sanwariya Packaging supports pharmaceutical companies in developing secure packaging solutions that help protect medicines across global markets.

Counterfiet_medcines

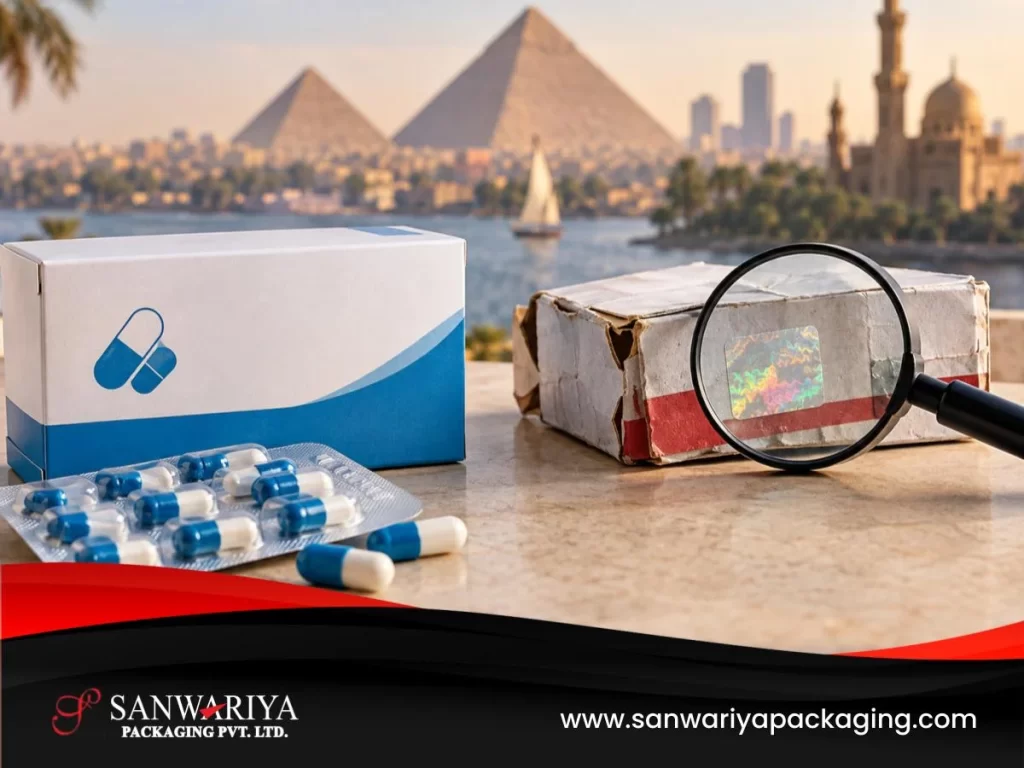
Counterfeit medicines in Egypt are a supply-chain problem, a regulatory problem and a packaging problem all at once. When a falsified product reaches a pharmacy shelf, it can pass for a genuine medicine to almost everyone who handles it. That makes packaging the first thing a counterfeiter copies and the first thing a brand owner must be able to defend.

For pharmaceutical manufacturers, brand owners and regulatory teams, the question is how to make genuine packaging harder to imitate and easier to verify, not only how to detect fakes after the fact.

This blog explains the counterfeit landscape in Egypt, how falsified products enter pharmaceutical supply chains, where packaging is vulnerable, and how secure foil and product identification fit into a broader anti-counterfeit strategy.

Counterfeit medicines in Egypt are best addressed through layered protection: secure primary packaging such as hologram and printed foils, serialization and track-and-trace, controlled distribution, and verification tools that pharmacists and patients can actually use.

Understanding the Counterfeit Medicine Landscape in Egypt

Counterfeit or falsified medicines are products that deliberately misrepresent their identity, composition or source. They may contain no active ingredient, the wrong dose, a different ingredient, or harmful contaminants, while carrying the name and appearance of a trusted brand.

The World Health Organization estimates that at least 1 in 10 medicines in low- and middle-income countries are substandard or falsified. This is an estimate for low- and middle-income countries and should not be interpreted as an Egypt-specific statistic. This is a global or regional estimate and should not be interpreted as an Egypt-specific statistic. Egypt, like other markets with complex pharmaceutical supply chains, continues to strengthen systems designed to improve product identification, traceability and regulatory oversight.

Egypt has also strengthened pharmaceutical traceability through the Egyptian Track & Trace System (EPTTS), overseen by the Egyptian Drug Authority (EDA). Under the Phase 1 technical requirements published in 2026, serialization is mandatory at the secondary-packaging level, with EPTTS requiring a Data Matrix ECC 200 containing key product information such as GTIN, serial number, expiry date and batch/lot. Manufacturers and exporters should verify the latest EDA requirements before finalizing packaging artwork, serialization workflows or security features.

Common risk categories in markets like Egypt include:

  • High-demand chronic and lifestyle medicines
  • Products affected by shortages or price gaps
  • Medicines sold through informal or unverified channels
  • Brands with strong reputations and visible packaging

How Counterfeit Products Enter Pharmaceutical Supply Chains

Counterfeit products rarely arrive through one obvious door. They typically enter wherever visibility is lowest.

Common entry points include:

  • Unauthorized or unlicensed distributors and intermediaries
  • Parallel trade and repackaging outside controlled channels
  • Diversion and re-entry of genuine, expired or returned stock
  • Online sales and informal retail outlets
  • Cross-border movement through less-monitored routes

The longer and more fragmented the supply chain, the more handover points exist where a falsified pack can be swapped in. This is why supply-chain transparency and packaging security have to work together.

Packaging Vulnerabilities That Can Enable Imitation

Counterfeiters are not copying the medicine first. They are copying what people see and trust: the carton, the blister card and the printed foil. Packaging that is easy to reproduce is easy to fake.

Typical packaging vulnerabilities include:

  • Standard printed foil with no unique security feature
  • Simple printing that can be replicated with commercial equipment
  • Cartons and leaflets that can be reproduced more easily than primary packaging
  • Absence of covert or machine-readable identifiers
  • Unclear visual cues that pharmacists and patients cannot easily check

The closer a security feature sits to the medicine itself, the harder it is to remove, reuse or convincingly imitate.

This is why primary packaging, especially the blister foil that directly seals each dose, is an important place to add protection. A carton can be replaced. A foil that carries integrated security features is far harder to duplicate.

Why Authentication and Product Identification Matter

Protection only works if someone can check it. Authentication turns packaging from a passive container into an active line of defense.

Effective authentication generally combines several layers:

  • Overt features: visible to the naked eye, such as holograms and distinctive foil patterns, for quick checks by pharmacists and patients
  • Covert features: hidden marks or inks that trained inspectors or tools can verify
  • Digital identifiers: serialized identifiers such as 2D Data Matrix codes, which can connect individual packs with traceability systems and product information.
  • Batch-level traceability: consistent batch, manufacturing and expiry information that can be cross-checked
A pack that can be identified, traced and verified gives regulators, distributors and patients something concrete to rely on, and gives brand owners evidence when a suspect product is found.

Regulatory and Supply-Chain Considerations

Packaging decisions for the Egyptian market should be made with regulators and the supply chain in mind, not just the artwork team.

Key considerations for manufacturers and exporters include:

  • Alignment with current EDA registration, labeling and EPTTS serialization requirements, including applicable secondary-packaging identification requirements
  • Compatibility of security features with high-speed blister packaging lines
  • Consistent artwork control, including Arabic and multilingual text requirements
  • Documented supplier qualification and quality agreements for packaging materials
  • Coordination between packaging, regulatory, QA/QC and supply-chain teams

Security features must also be practical. A feature that disrupts sealing performance, print registration or line speed will not survive production, however impressive it looks.

The Role of Secure Packaging in a Broader Anti-Counterfeit Strategy

No single feature stops counterfeiting. Secure packaging is one layer in a wider strategy that also includes serialization, distributor control, market surveillance, staff training and cooperation with authorities.

Where packaging contributes most:

  • Deterrence: advanced foil features raise the cost and difficulty of copying
  • Detection: overt and covert features give inspectors and pharmacists a fast way to spot suspect products
  • Protection of integrity: strong, consistent foil structures keep the medicine protected until the moment of use
  • Brand confidence: visible security reassures healthcare professionals and patients
The most effective approach layers these features so that a counterfeiter would have to defeat several at once.

How Sanwariya Packaging Supports Anti-Counterfeit Strategies

Sanwariya Packaging is a manufacturer and exporter of pharmaceutical aluminum foils, both unprinted and printed, built for reliable barrier performance, consistent sealing and stable print quality.

For brand owners concerned about imitation, relevant options include:

Through controlled manufacturing and strict quality processes, Sanwariya works with pharmaceutical companies to develop foil solutions that combine protection, printability and security for demanding export markets.

Ready to strengthen your packaging against counterfeiting? Get in touch with our team or request a quote.

Related Blogs

Importance of strong foil in pharmacy dispensing

Modern pharmaceutical supply chains often extend across continents. Medicines manufactured in one country may travel thousands of kilometers before reaching distributors, pharmacies, and ultimately patients. During this journey, pharmaceutical products may face fluctuating temperatures, high humidity levels, mechanical stress, and prolonged storage conditions.

For formulations containing sensitive Active Pharmaceutical Ingredients (APIs), these environmental factors can pose significant stability risks. As a result, packaging plays a critical role in maintaining product quality throughout global logistics networks. Selecting the correct blister foil structure helps ensure that medicines remain safe, effective, and stable even after long transit periods.

Why Long Supply Chains Create Stability Challenges

Unlike many consumer products, pharmaceutical medicines must maintain strict quality and stability parameters from manufacturing to patient use. Long-distance transportation introduces multiple stages where environmental conditions may vary.

Shipments frequently move through trucks, shipping containers, cargo aircraft, and distribution warehouses. At each stage, exposure to temperature variation, humidity, and mechanical vibration can occur. Over time, these environmental stresses may affect both the packaging and the product inside.

For APIs that are sensitive to moisture, oxygen, or light, inadequate packaging protection can increase the risk of degradation during transit. Therefore,  pharmaceutical packaging must be designed not only for storage stability but also for real-world supply chain conditions.

Supply Chain Journey Conditions

International pharmaceutical distribution often involves complex logistics routes. A single shipment may move through several countries, climate zones, and transportation modes before reaching the final destination.

Sea freight, which is commonly used for global pharmaceutical distribution, can take several weeks depending on the route. During this period, containers may experience high humidity levels, especially when traveling through tropical or coastal regions.

In addition to environmental exposure, products may also remain in temporary storage at ports, warehouses, and customs facilities. These extended holding periods increase the importance of packaging materials that can maintain strong barrier performance over time.

Understanding the complete supply chain journey helps packaging teams select materials capable of protecting pharmaceutical products during prolonged logistics timelines.

The Role of Humidity Protection

Humidity is one of the most significant environmental threats to pharmaceutical stability during long-distance transportation. Many APIs are sensitive to moisture and can undergo hydrolysis reactions when exposed to elevated humidity levels.

Even small amounts of water vapor entering blister cavities can gradually affect product stability over extended transit periods. High humidity environments combined with long shipping durations can accelerate degradation processes if packaging barriers are insufficient.

High-barrier aluminum blister foils significantly reduce moisture vapor transmission, helping protect the internal environment of each blister cavity. By maintaining a stable microenvironment around the medicine, these barrier materials play a crucial role in preserving API integrity during international shipping.

Mechanical Stress During Transportation

Pharmaceutical products encounter repeated handling throughout the supply chain. Cartons are stacked on pallets, transported by trucks, transferred between warehouses, and loaded onto ships or aircraft.

These operations introduce vibrations, compression forces, and occasional impacts that can stress packaging structures. If blister packs lack adequate mechanical strength, cavities may deform or seals may weaken, potentially allowing environmental intrusion.

Durable pharmaceutical foil structures help maintain seal integrity and cavity stability even under challenging logistics conditions. Strong blister materials reduce the likelihood of packaging damage and help ensure that each dose remains properly protected until it reaches the patient.

Selecting the Correct Barrier Structure

Packaging engineers must evaluate several factors when selecting blister foil structures for products intended for long-distance export. The sensitivity of the API, expected transit duration, and environmental conditions along the shipping route all influence packaging requirements.

Standard blister foil structures may be suitable for domestic distribution or short supply chains. However, products shipped across international routes often require enhanced barrier performance.

Aluminum-based blister foils provide excellent protection against moisture, oxygen, and light. These materials are commonly used for formulations that require high levels of environmental protection during storage and transportation.

By aligning packaging design with logistics realities, pharmaceutical companies can significantly reduce the risk of stability issues during transit.

Packaging Considerations for Export Markets

Global pharmaceutical distribution requires careful coordination between formulation scientists, packaging development teams, and supply chain specialists. Export markets may present environmental conditions that differ significantly from domestic storage environments.

Certain regions experience consistently high humidity, while others may have extreme seasonal temperatures. These environmental variations must be considered when qualifying packaging systems for international distribution.

High-barrier blister packaging helps maintain product stability despite these environmental differences. Reliable packaging solutions support consistent medicine quality regardless of how far the product must travel before reaching healthcare providers and patients.

Maintaining API Stability Across Global Supply Chains

Long-distance pharmaceutical distribution exposes medicines to humidity, temperature changes, mechanical vibration, and extended storage timelines. Effective blister packaging plays a critical role in protecting sensitive APIs from these environmental risks during international transportation.

By selecting high-barrier pharmaceutical foil structures with strong moisture protection and mechanical durability, pharmaceutical manufacturers can maintain product stability throughout complex logistics networks. Proper packaging selection helps ensure medicines retain their safety, potency, and quality from manufacturing facilities to patients worldwide.

Sanwariya Packaging manufactures pharmaceutical aluminum foils designed to provide strong moisture barriers, consistent sealing performance, and reliable mechanical stability for blister packaging applications. Through advanced manufacturing processes and strict quality controls, Sanwariya Packaging supports pharmaceutical companies in protecting API stability across long global supply chains and challenging transit environments.

Packaging strategies to protect APIs across supply chains

Pharmaceutical packaging must protect medicines not only during manufacturing and transportation but also during the final stages of the supply chain. One of the most demanding environments for packaging materials is the pharmacy dispensing stage. 

In hospitals, retail pharmacies, and clinical settings, blister packs are frequently handled by pharmacists, technicians, and patients. During this stage, packaging materials are exposed to repeated handling, pressure, and mechanical stress. 

If blister foils are not sufficiently durable, they may tear prematurely, puncture easily, or compromise the protection of the medicine inside. Because of this, the mechanical strength and durability of pharmaceutical foil are critical considerations during packaging development. 

This blog explains why durable blister foils are important in pharmacy environments, how tear strength and puncture resistance contribute to packaging performance, and how pharmaceutical companies ensure that packaging materials remain reliable throughout dispensing and patient use.

Packaging Stress in Pharmacy Dispensing Environments

Pharmacy dispensing environments involve frequent manual handling of medicine packs. Pharmacists and technicians often remove individual doses from larger packaging units, verify labeling information, and prepare medicines for patient distribution.

During these routine activities, blister packs may experience several types of mechanical stress.

  • Repeated bending or flexing of blister cards
  • Pressure applied while separating doses
  • Contact with dispensing equipment or storage trays
  • Handling during patient counseling and medication preparation

These handling conditions can place significant strain on blister foil structures. If the foil material is too fragile, it may tear unintentionally or fail to maintain the integrity of the blister cavity.

Durable foil materials help ensure that the packaging continues to protect the medicine until the moment of use.

Importance of Tear Strength in Blister Foils

Tear strength refers to the ability of a material to resist tearing when a force is applied. In pharmaceutical blister packaging, appropriate tear strength is necessary to maintain packaging integrity while still allowing the medicine to be dispensed intentionally.

If foil tear strength is too low, several problems may occur:

  • Accidental Tearing During Routine Handling
  • Exposure Of The Medicine Before Intended Use
  • Reduced Protection From Environmental Factors
  • Potential Contamination Risks

On the other hand, foil should not be excessively difficult to open. Packaging must balance durability with accessibility to ensure that patients can remove medicines without excessive effort.

Packaging engineers therefore design foil structures that provide controlled tearing during the push-through dispensing process.

Puncture Resistance and Blister Protection

Puncture resistance is another important property of durable blister foil. This refers to the ability of the material to resist penetration by external pressure or sharp contact.

During pharmacy handling and transportation, blister packs may be exposed to objects that apply localized pressure.

Examples may include:

  • Contact With Sharp Edges Of Storage Trays
  • Compression Within Medication Carts
  • Stacking Of Packaged Medicines
  • Accidental Impacts During Handling

If the foil surface punctures easily, the protective barrier around the medicine may be compromised.

Foils with strong puncture resistance help maintain the protective seal around each blister cavity and reduce the risk of accidental exposure.

Balancing Durability and Patient Accessibility

Pharmaceutical packaging must remain strong enough to protect the product while still allowing patients to access the medicine easily.

Designing blister foils requires careful consideration of patient usability factors.

Key design considerations include:

  • Controlled Push-Through Performance
  • Resistance To Accidental Tearing During Handling
  • Accessibility For Elderly Or Limited-Strength Patients
  • Consistent Opening Performance Across Blister Cavities

Packaging development teams often conduct usability evaluations to ensure that the blister pack remains easy to open without compromising durability.

Achieving this balance helps support safe and convenient medication use.

Mechanical Stability During High-Volume Pharmacy Use

In hospital pharmacies and large dispensing centers, medicines may be handled in high volumes every day. Blister packs are frequently stored in automated dispensing cabinets, medication carts, or inventory trays.

These environments place repeated mechanical stress on packaging materials.

Potential stress factors include:

  • Frequent Insertion And Removal From Storage Systems
  • Vibration During Movement Of Dispensing Carts
  • Pressure From Stacked Packaging Units
  • Repeated Manual Handling By Pharmacy Staff

Foil structures with strong mechanical stability help maintain packaging performance even under these demanding conditions.

Reliable packaging durability supports smooth pharmacy operations and reduces the risk of damaged medicine packs.

Quality Testing for Foil Durability

Before  pharmaceutical packaging materials are approved for production use, they typically undergo testing to evaluate mechanical strength and durability.

These tests help confirm that the foil structure can withstand expected handling conditions throughout the supply chain.

Common durability evaluations may include:

  • Tear Resistance Testing
  • Puncture Resistance Measurements
  • Push-Through Force Testing For Blister Packs
  • Simulated Handling And Transport Tests

Quality assurance teams review the results of these tests to ensure that packaging materials meet both functional and regulatory expectations.

Maintaining documented testing procedures also supports compliance with pharmaceutical quality systems.

Ensuring Safe Dispensing and Patient Protection

Durable blister foil plays an important role in maintaining the integrity of  pharmaceutical packaging from production to patient use. In pharmacy environments where medicines are frequently handled, strong foil materials help prevent accidental damage and preserve the protective barrier around each dose.

By combining appropriate tear strength, puncture resistance, and controlled opening performance, pharmaceutical packaging can remain reliable throughout dispensing and patient use.

Durable foil structures contribute to safe medication handling, clear product identification, and consistent packaging performance across healthcare environments.

Sanwariya Packaging manufactures pharmaceutical aluminum foils designed to provide reliable mechanical strength, consistent sealing performance, and stable printing quality for blister packaging applications. Through advanced manufacturing processes and strict quality controls, Sanwariya Packaging supports pharmaceutical companies in developing durable packaging solutions suitable for demanding pharmacy dispensing environments.

Proper handling, storage, and transport of pharma foil

Pharmaceutical products distributed internationally must comply with labeling regulations across multiple countries. In many markets, medicines are required to display information in more than one language to ensure that patients and healthcare professionals clearly understand product details and usage instructions. 

As a result, pharmaceutical packaging often needs to accommodate multilingual text while maintaining readability, regulatory compliance, and accurate information presentation. Printed aluminum blister foils frequently carry important product information such as medicine names, dosage strengths, batch details, manufacturing information, and storage instructions. 

When these details must appear in multiple languages, careful layout design becomes essential. Font size, text spacing, line order, and translation accuracy must all be managed to ensure that information remains clear and compliant. 

This blog explains how pharmaceutical companies design foil text layouts for multilingual export markets and highlights the importance of font selection, regulatory text structure, and error-free translations in multilingual pharma foil printing.

Why Multilingual Packaging Is Required in Global Markets

Pharmaceutical companies exporting medicines to international markets must follow the labeling requirements established by local regulatory authorities. Many regions require medicines to display product information in multiple languages to support safe usage and patient understanding.

Multilingual packaging helps ensure that essential product information is accessible to a diverse population.

Common reasons for multilingual labeling include:

  • Regulatory requirements in multilingual regions
  • Patient safety and accessibility considerations
  • Clear communication for healthcare professionals
  • Standardized labeling across export markets

Countries or regions with multiple official languages often require bilingual or multilingual labeling to ensure that product information is understood by all users.

When blister foils contain printed product information, the layout must accommodate these language requirements without compromising readability.

Challenges of Multilingual Text on Blister Foils

Blister foils have limited printable space, especially when compared with outer cartons or patient information leaflets. This limited surface area makes multilingual layout design more complex.

Adding multiple languages to the same foil requires careful planning to ensure that each line of text remains readable and correctly aligned.

Common challenges include:

  • Limited space for multiple language blocks
  • Variations in word length between languages
  • Maintaining clear spacing between text lines
  • Preserving readability on small blister cavities
Packaging development teams must design layouts that balance space constraints with regulatory labeling requirements. Proper planning during the artwork stage helps prevent overcrowded or difficult-to-read packaging.

Font Size and Spacing Considerations

Maintaining readable text is one of the most important aspects of multilingual pharmaceutical labeling. Font sizes must be large enough to remain legible while still fitting within the available print area on the foil.

Several design considerations help maintain readability:

  • Consistent font sizes across languages
  • Adequate spacing between lines of text
  • Clear separation between language sections
  • Avoidance of overly condensed fonts
Spacing becomes particularly important when multiple languages appear on a single foil surface. If text is too closely spaced, it may become difficult to read after printing or during product handling. Packaging artwork teams therefore evaluate layout designs carefully before finalizing the print artwork.

Regulatory Line Order and Information Hierarchy

Regulatory guidelines often specify the order in which certain information must appear on pharmaceutical packaging. This includes elements such as the product name, dosage strength, manufacturing details, batch number, and expiration date.

When designing multilingual layouts, the structure of this information must remain consistent across all languages.

Typical layout considerations may include:

  • Placing critical product identification details in a prominent position
  • Maintaining the same information sequence across languages
  • Ensuring regulatory text remains clearly visible
  • Avoiding overlap between different language blocks

Maintaining a logical information hierarchy helps ensure that healthcare professionals and patients can quickly identify important product details.

Packaging designs must therefore balance regulatory structure with available print space.

Preventing Translation Errors in Packaging Artwork

Accurate translation is essential when pharmaceutical packaging is printed in multiple languages. Even small translation errors can create confusion or lead to regulatory compliance issues.

To prevent such risks, pharmaceutical companies often follow structured translation verification processes.

These processes may include:

  • Professional medical translation services
  • Review by regulatory or medical specialists
  • Cross-checking translations against approved product documentation
  • Final proofreading before artwork approval

Because blister foils are printed in large production volumes, translation accuracy must be confirmed before printing begins.

Correcting errors after production can result in material waste or packaging delays.

Printing Precision and Layout Stability

Printing multilingual text on aluminum foil requires precise alignment and consistent print quality. Small variations in print registration or layout alignment may affect text readability, especially when multiple language blocks appear close together.

Production teams monitor several factors to maintain layout accuracy:

  • Precise printing registration across foil reels
  • Stable ink density for small text characters
  • Controlled printing pressure to maintain clarity
  • Consistent alignment of repeated blister patterns

Maintaining stable printing conditions ensures that multilingual text remains clear and readable across the entire production batch.

Reliable printing processes are therefore essential for high-quality multilingual pharma foil printing.

Export Market Considerations for Multilingual Packaging

Pharmaceutical companies supplying medicines to multiple regions often manage several packaging variations to meet local language requirements.

Export teams work closely with packaging and regulatory departments to ensure that each market receives compliant packaging.

Important considerations for export packaging may include:

  • Adapting packaging artwork for region-specific language requirements
  • Ensuring translations meet local regulatory guidelines
  • Managing multiple artwork versions for different markets
  • Maintaining consistency across packaging materials

These processes help ensure that medicines distributed internationally meet both regulatory expectations and patient communication needs.

Supporting Clear Communication Across Global Markets

Multilingual pharmaceutical packaging plays an important role in ensuring that medicine information is accessible to patients and healthcare professionals around the world. Designing foil text layouts for multiple languages requires careful attention to font sizing, spacing, information hierarchy, and translation accuracy.

By following structured artwork design practices and maintaining precise printing control, pharmaceutical companies can produce packaging that remains clear, compliant, and easy to read across international markets.

Effective multilingual labeling helps reduce communication barriers and supports safe medicine use in diverse healthcare environments.

Sanwariya Packaging manufactures printed pharmaceutical aluminum foils designed to support precise text reproduction, consistent print alignment, and high-quality multilingual printing. Through advanced printing capabilities and controlled production processes, Sanwariya Packaging helps pharmaceutical companies deliver packaging solutions that maintain clarity and regulatory compliance across global export markets.

Designing foil text for multi-language markets

Pharmaceutical aluminum foil is a critical packaging material used in blister packaging to protect medicines from moisture, oxygen, light, and external contamination. While foil structures are designed to provide strong barrier performance, their protective properties must be preserved throughout the supply chain. 

Improper handling, storage, or transportation can damage the foil surface, affect sealing performance, or compromise print quality. Because of this, pharmaceutical companies follow strict procedures when storing and transporting foil reels. 

Controlled environmental conditions, careful reel handling, and systematic inspection help ensure that packaging materials remain in optimal condition before entering the packaging line. 

This blog explains recommended pharma foil storage guidelines, including temperature and humidity control, proper reel handling practices, transportation considerations, and inspection procedures for incoming materials.

Why Proper Handling of Pharma Foil Matters

Pharmaceutical foil is manufactured under controlled conditions to meet strict quality and barrier performance requirements. However, the material can still be affected by environmental exposure or physical damage during storage and transportation.

Improper foil handling may lead to several issues:

  • Dents or deformation of foil reels
  • Damage to printed surfaces
  • Contamination of the foil surface
  • Reduced sealing performance during blister packaging

Even minor physical damage can affect packaging line performance. For example, uneven reels may cause feeding problems during high-speed blister packaging operations.

Maintaining proper handling procedures helps preserve the structural integrity and print quality of the foil.

Temperature and Humidity Control for Foil

Environmental conditions play an important role in maintaining the quality of pharmaceutical packaging materials. Excessive humidity or temperature fluctuations may affect coatings, adhesives, or printing layers applied to the foil.

Warehouses storing pharmaceutical foils typically maintain controlled environmental conditions.

Important environmental controls for foil include:

  • Stable temperature conditions within recommended storage ranges
  • Relative humidity control to prevent moisture exposure
  • Avoidance of direct sunlight or heat sources
  • Protection from sudden environmental fluctuations

Maintaining stable environmental conditions helps prevent condensation or surface degradation that could affect packaging performance.

Controlled storage environments also support compliance with pharmaceutical quality management systems.

Best Practices for Reel Handling

Pharmaceutical foil is usually supplied in large reels that must be handled carefully during transportation, storage, and transfer to packaging lines.

Improper handling may cause physical damage such as edge dents, crushed cores, or surface scratches.

Recommended reel handling practices include:

  • Using appropriate lifting equipment designed for reel handling
  • Avoiding rolling reels directly on warehouse floors
  • Protecting reel edges from impact damage
  • Keeping reels in their original protective packaging until use
Handling procedures should also ensure that the reels remain properly aligned to prevent deformation. Careful reel handling helps maintain smooth operation during blister packaging production.

Preventing Mechanical Damage During Storage

Mechanical damage is one of the most common causes of foil rejection during incoming material inspections.

Damage may occur when reels are stacked improperly or when heavy objects are placed on top of packaging materials.

Warehouses storing pharmaceutical foil typically follow several protective practices.

  • Storing reels vertically on stable pallets
  • Maintaining sufficient spacing between stacked materials
  • Preventing contact with sharp edges or heavy equipment
  • Ensuring stable stacking to avoid reel movement

Proper storage arrangements help protect both the foil surface and the structural integrity of the reel.

Maintaining clean and organized warehouse environments also reduces the risk of contamination.

Transportation and Logistics Considerations

Pharmaceutical foil often travels long distances before reaching the packaging facility. During transportation, packaging materials may be exposed to vibrations, environmental changes, or handling by multiple logistics providers.

To reduce these risks, foil reels are usually transported using protective packaging and secure palletization.

Key transportation considerations include:

  • Stable pallet stacking to prevent movement during transit
  • Protective wrapping to shield reels from dust and moisture
  • Shock protection to reduce vibration-related damage
  • Climate-aware transportation for sensitive materials

Export shipments may also require additional precautions, particularly when transporting materials through regions with extreme environmental conditions.

Proper logistics planning helps ensure that packaging materials arrive in usable condition.

Inspection of Foil Reels on Receipt

Quality control procedures typically require inspection of incoming packaging materials before they are released for production use.

Incoming inspection helps confirm that the materials received meet approved specifications and have not been damaged during transportation.

Common inspection checks may include:

  • Verification of reel identification and batch documentation
  • Visual inspection for dents, scratches, or surface damage
  • Confirmation of protective packaging integrity
  • Review of storage conditions during transport if required
If any issues are identified during inspection, the material may be placed on hold for further evaluation. These inspection steps help maintain quality control within pharmaceutical packaging operations.

Warehouse Inventory and Stock Rotation

Proper inventory management helps ensure that packaging materials are used within their recommended storage period.

Pharmaceutical warehouses often follow structured inventory systems that track material batches and storage durations.

Common inventory management practices include:

  • First-in, first-out (FIFO) material usage
  • Clear batch identification and labeling
  • Regular warehouse condition monitoring
  • Documentation of storage conditions and handling procedures

Following these practices ensures traceability and helps maintain packaging material performance throughout storage.

Inventory control is an important part of pharmaceutical quality management systems.

Maintaining Packaging Material Integrity Across the Supply Chain

Pharmaceutical packaging materials must maintain consistent quality from manufacturing to final use on packaging lines. Proper handling, storage, and transportation procedures help ensure that foil reels remain free from damage and environmental exposure.

Following established pharma foil storage guidelines supports reliable blister packaging performance, protects printing quality, and helps maintain regulatory compliance within pharmaceutical manufacturing environments.

Supply chain teams, warehouse managers, and quality control personnel all play an important role in protecting packaging materials throughout their lifecycle.

Sanwariya Packaging manufactures pharmaceutical aluminum foils designed for reliable barrier performance, stable printing, and compatibility with high-speed blister packaging systems. Through controlled manufacturing processes and secure packaging practices supported by its infrastructure, Sanwariya Packaging supports pharmaceutical companies in maintaining the integrity of packaging materials throughout global storage and distribution.

For further information or requirements, you can get in touch with us or directly request a quote.